



























California Proposition 65 Warning
 WARNING: This product may contain materials and/or chemicals such as arsenic, lead, and others that are known by the state of California to cause cancer and/or reproductive problems.
For more information, visit www.P65Warnings.ca.gov
Payment & Security
Méthodes de paiement
Vos informations de paiement sont gérées de manière sécurisée. Nous ne stockons ni ne pouvons récupérer votre numéro de carte bancaire.
Sécurité

Estimer la livraison
Informations produit supplémentaires
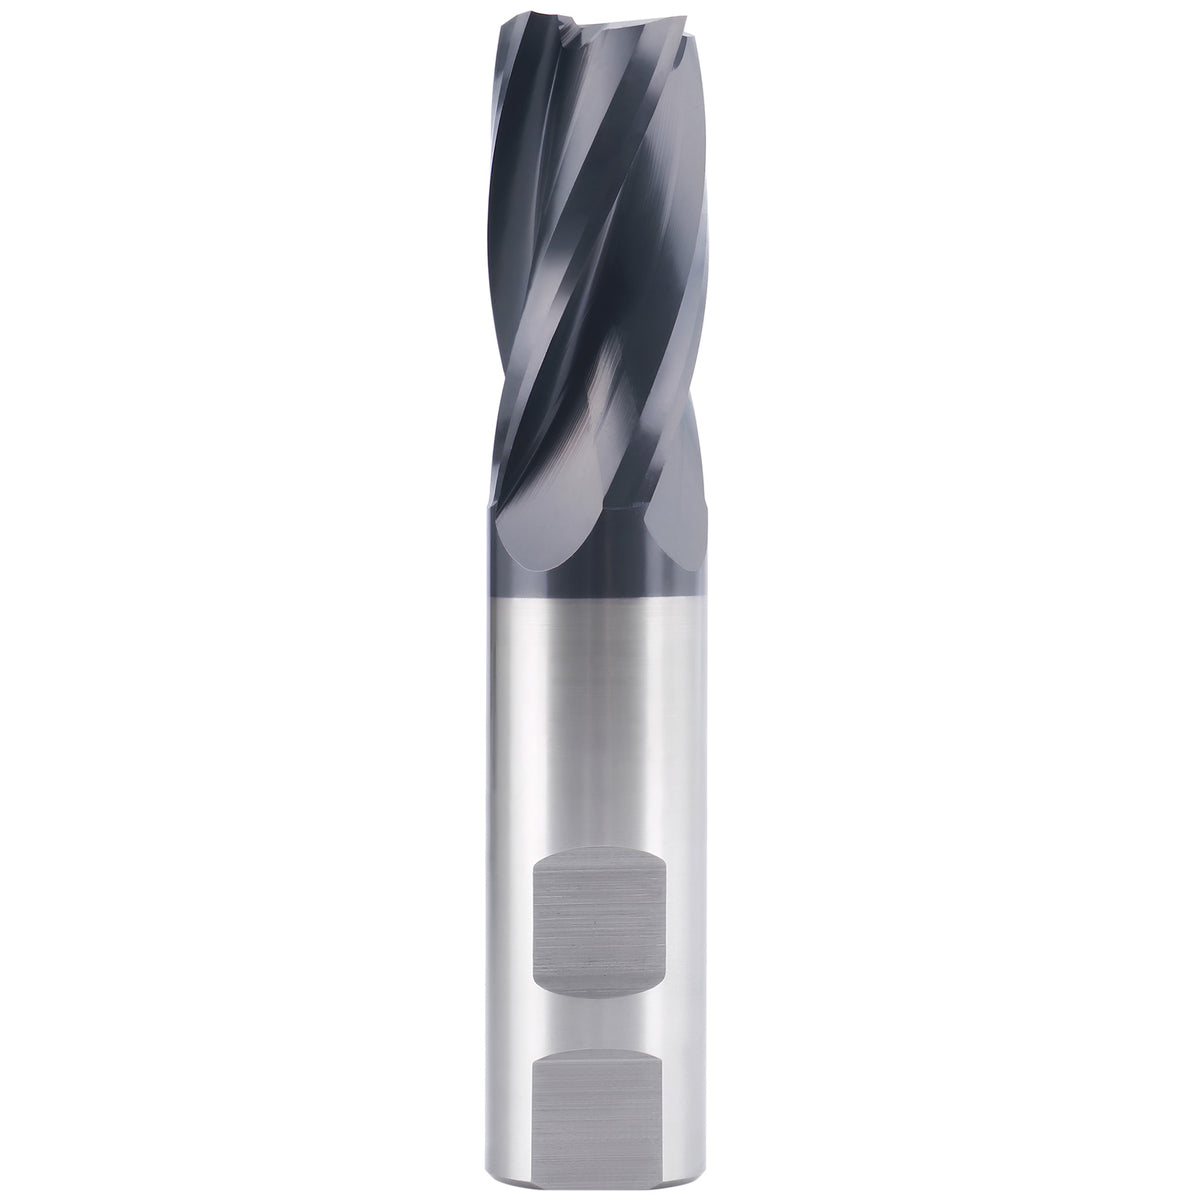
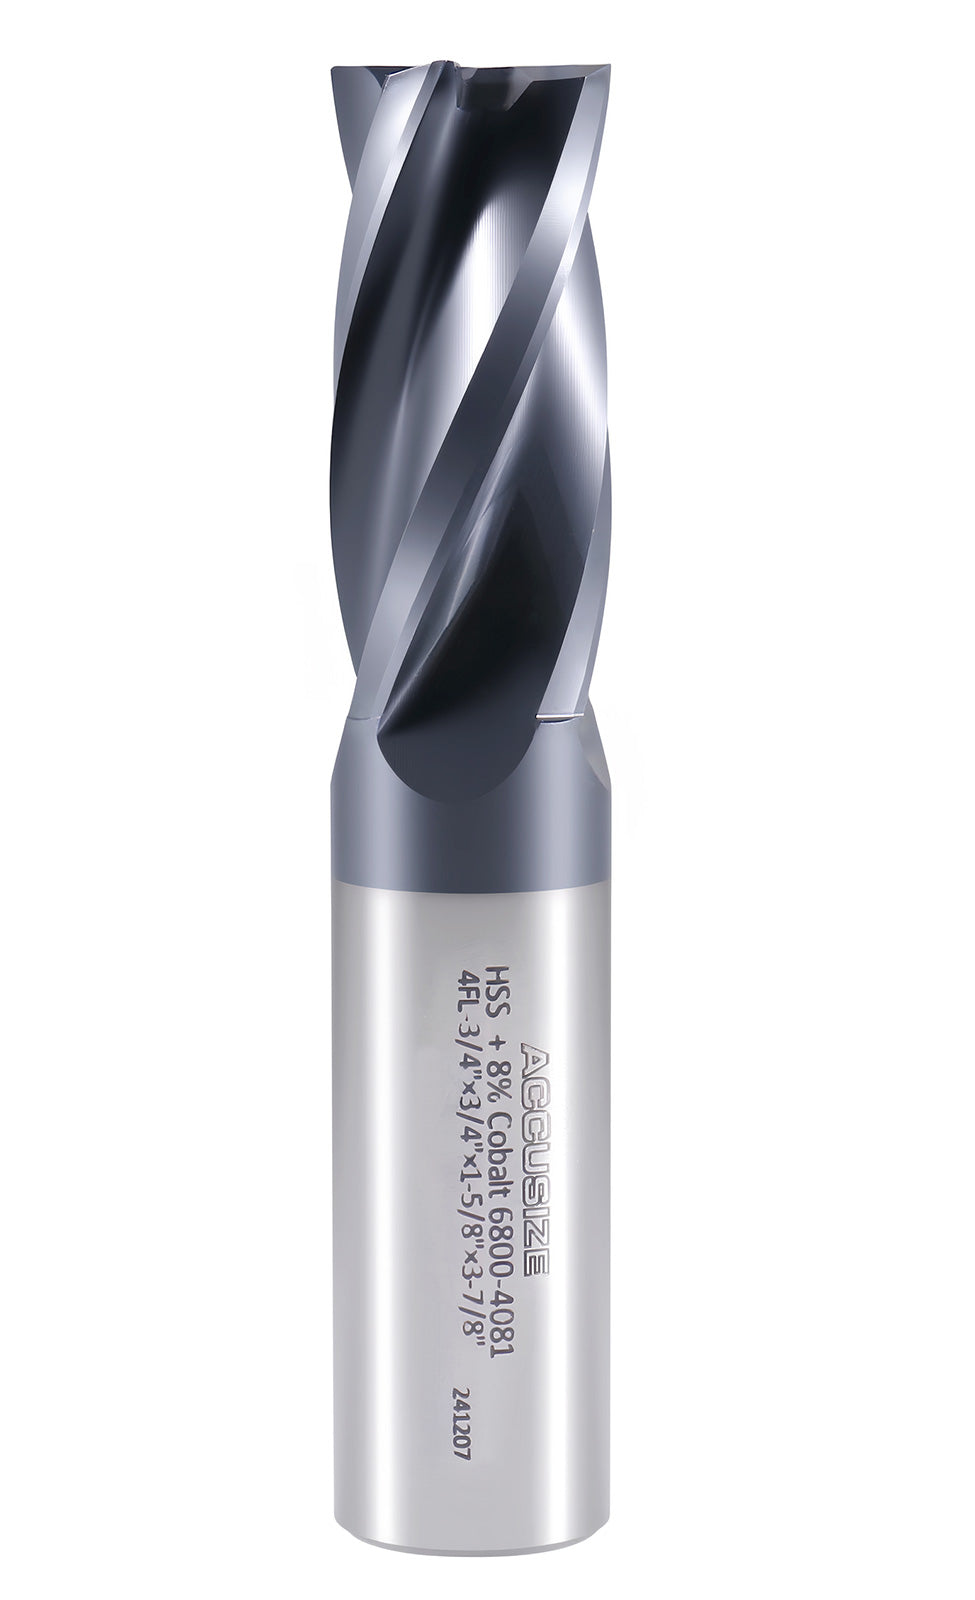
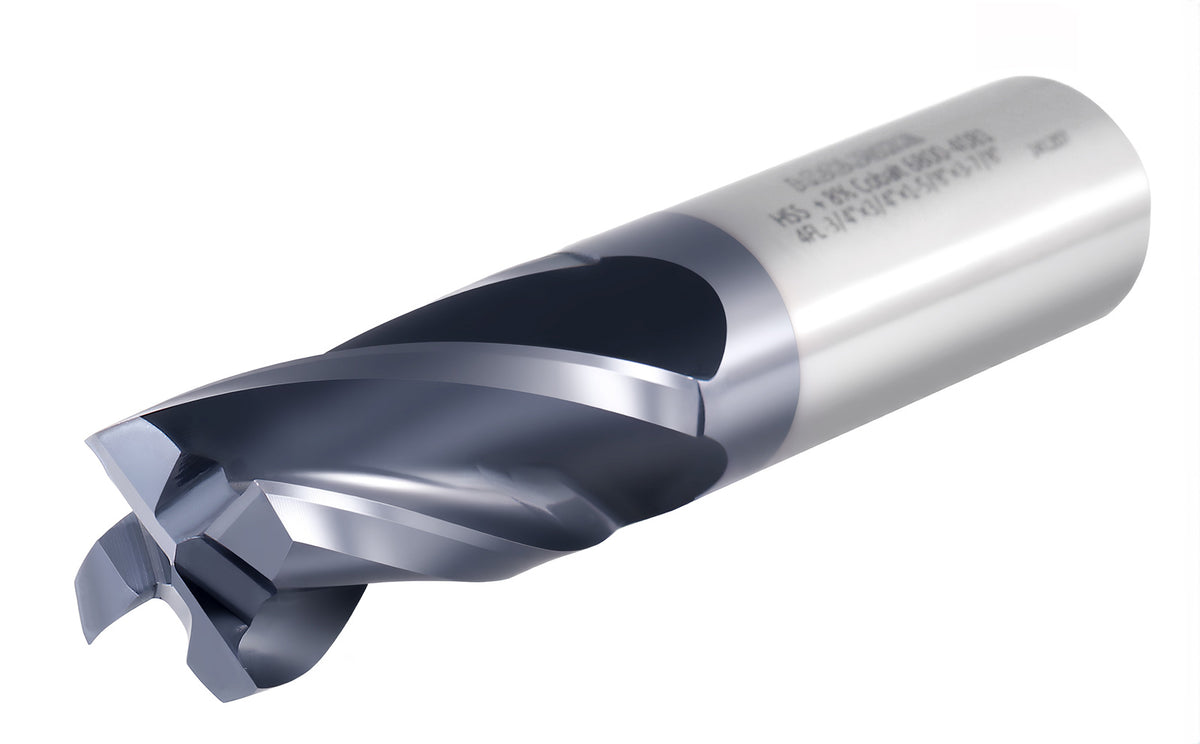
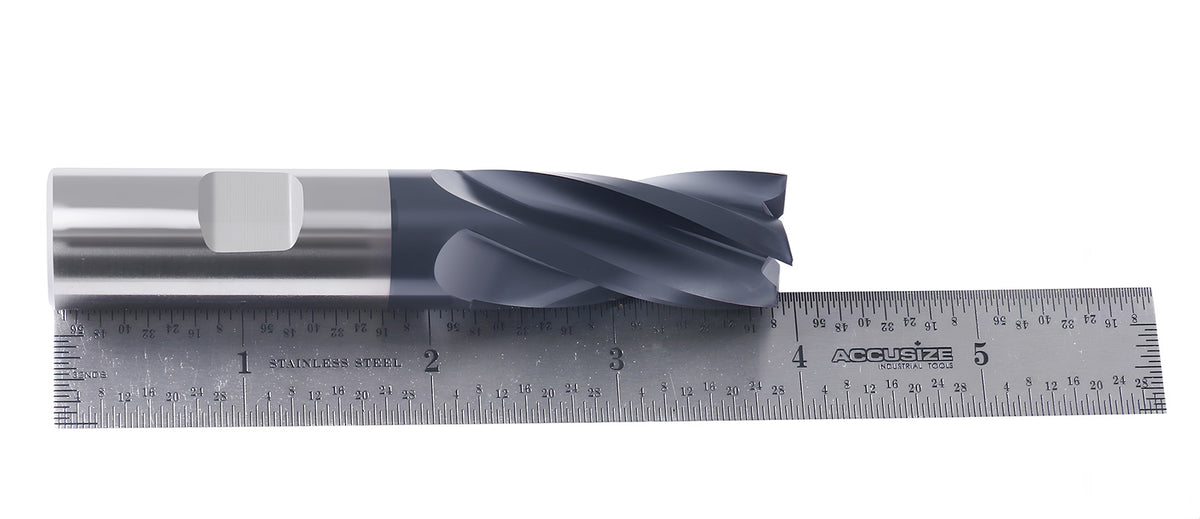
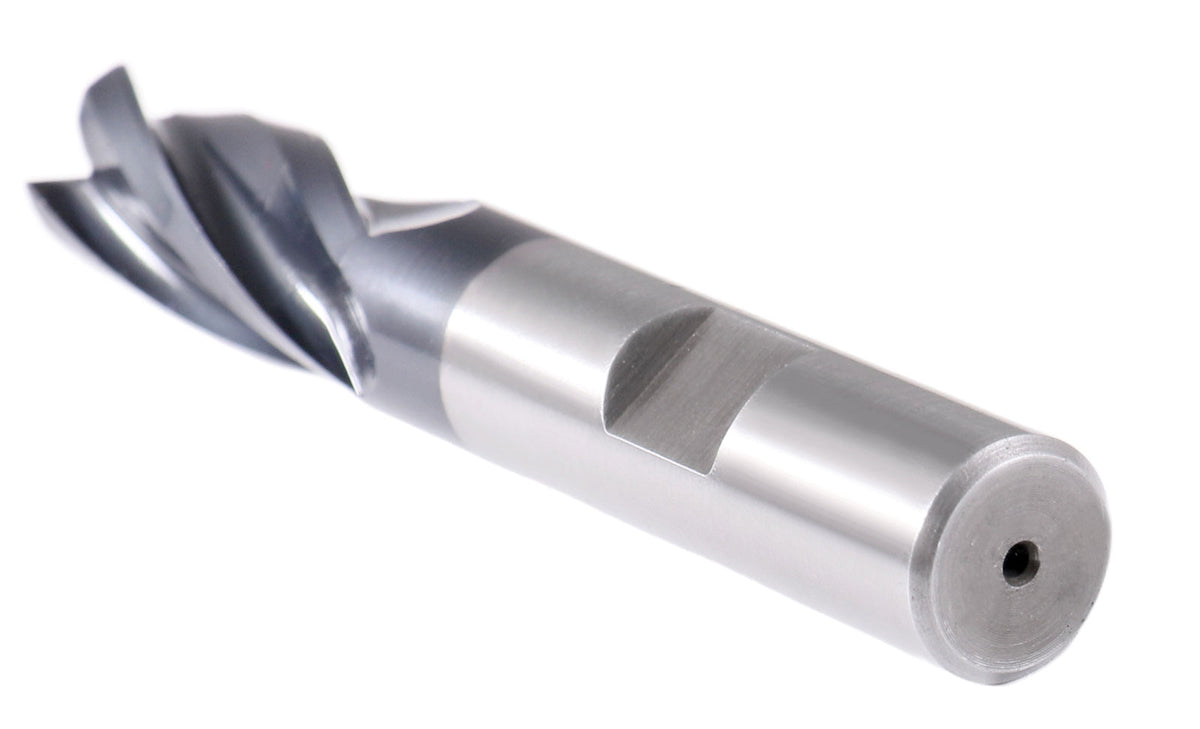
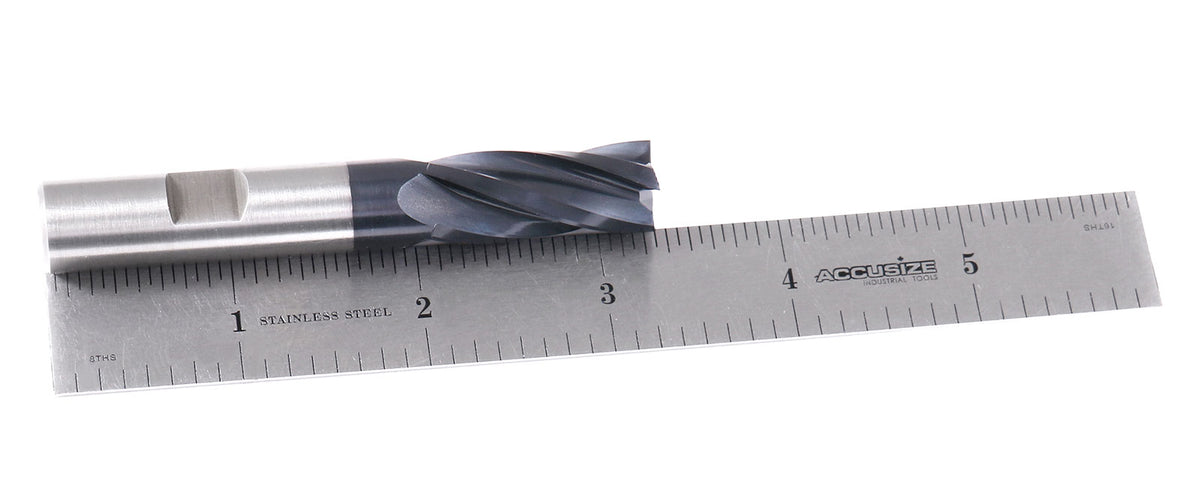
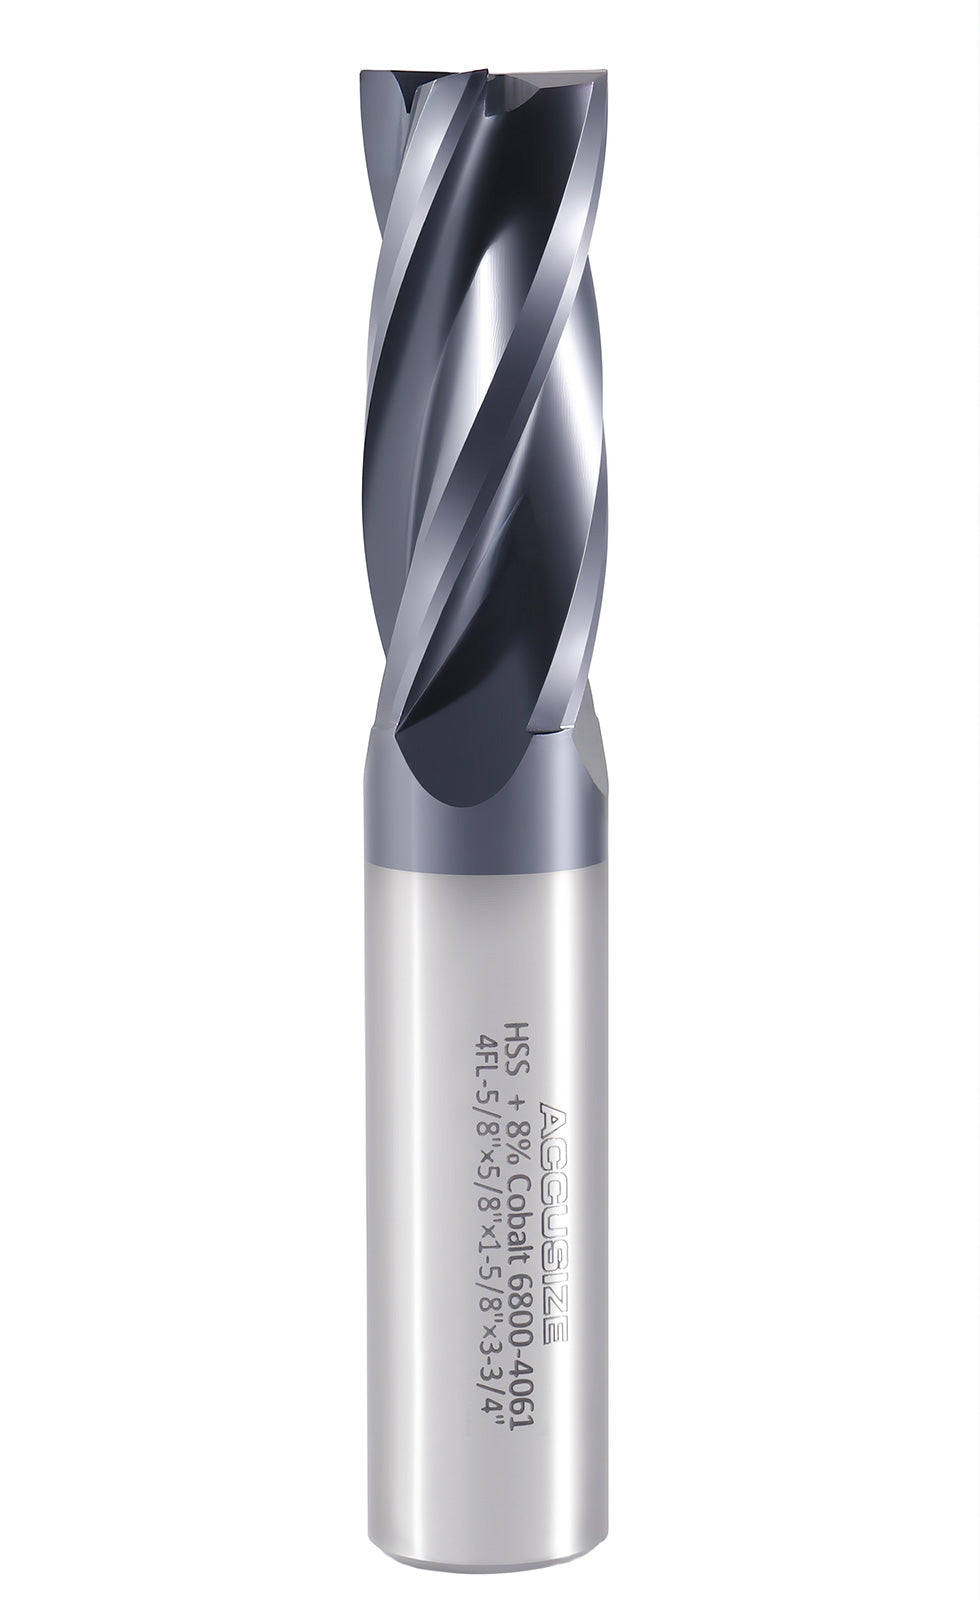
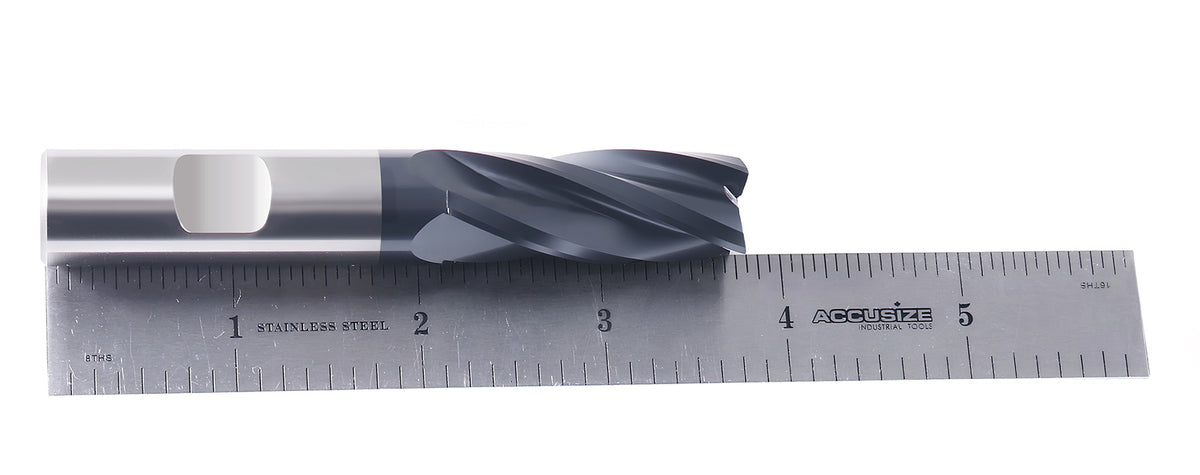
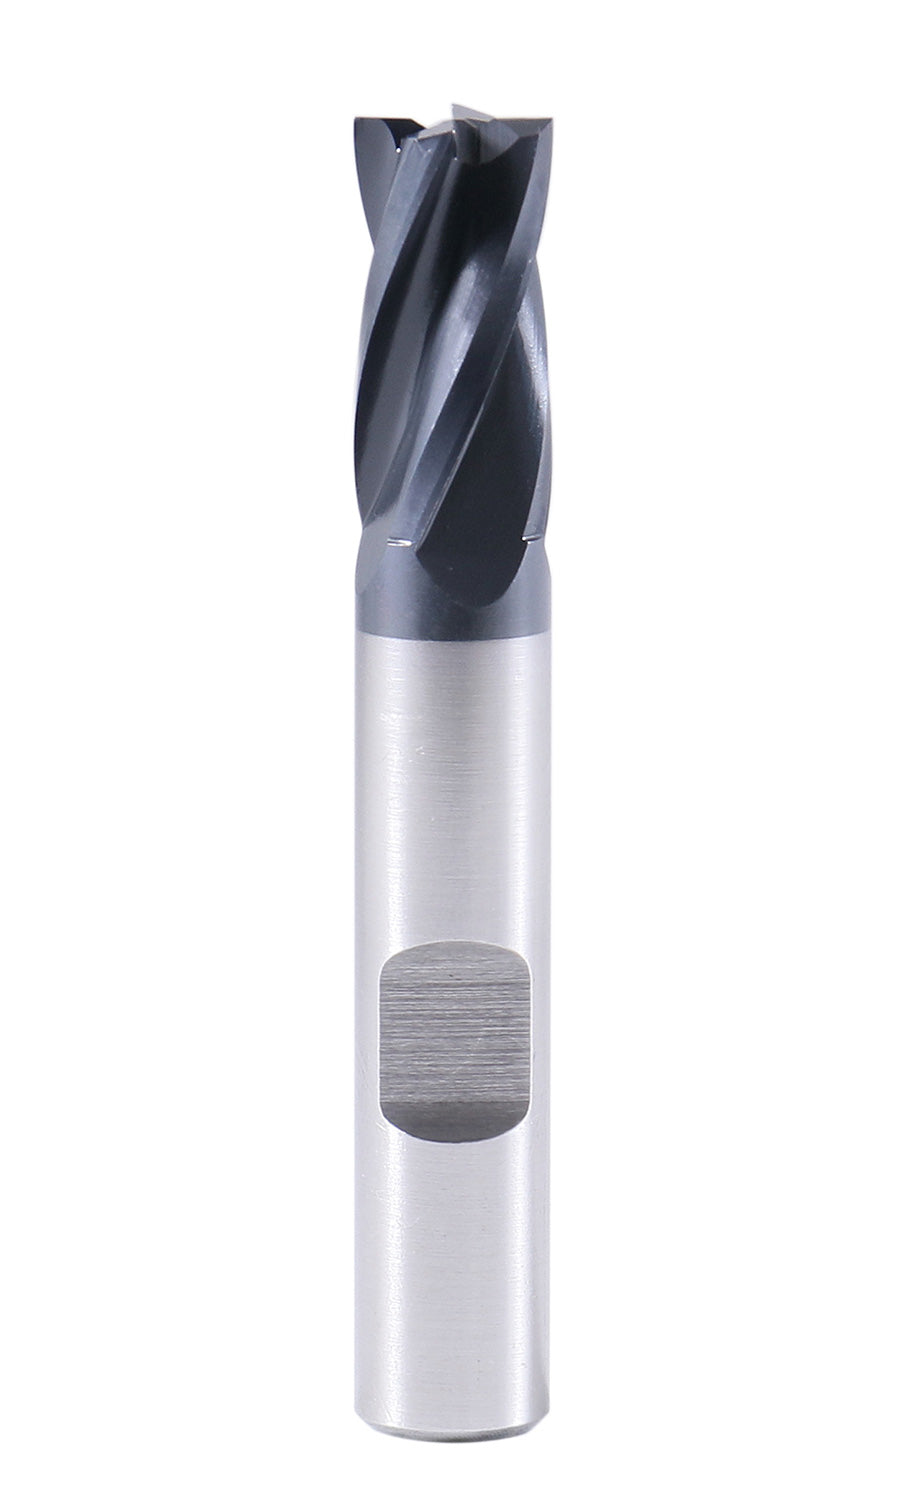
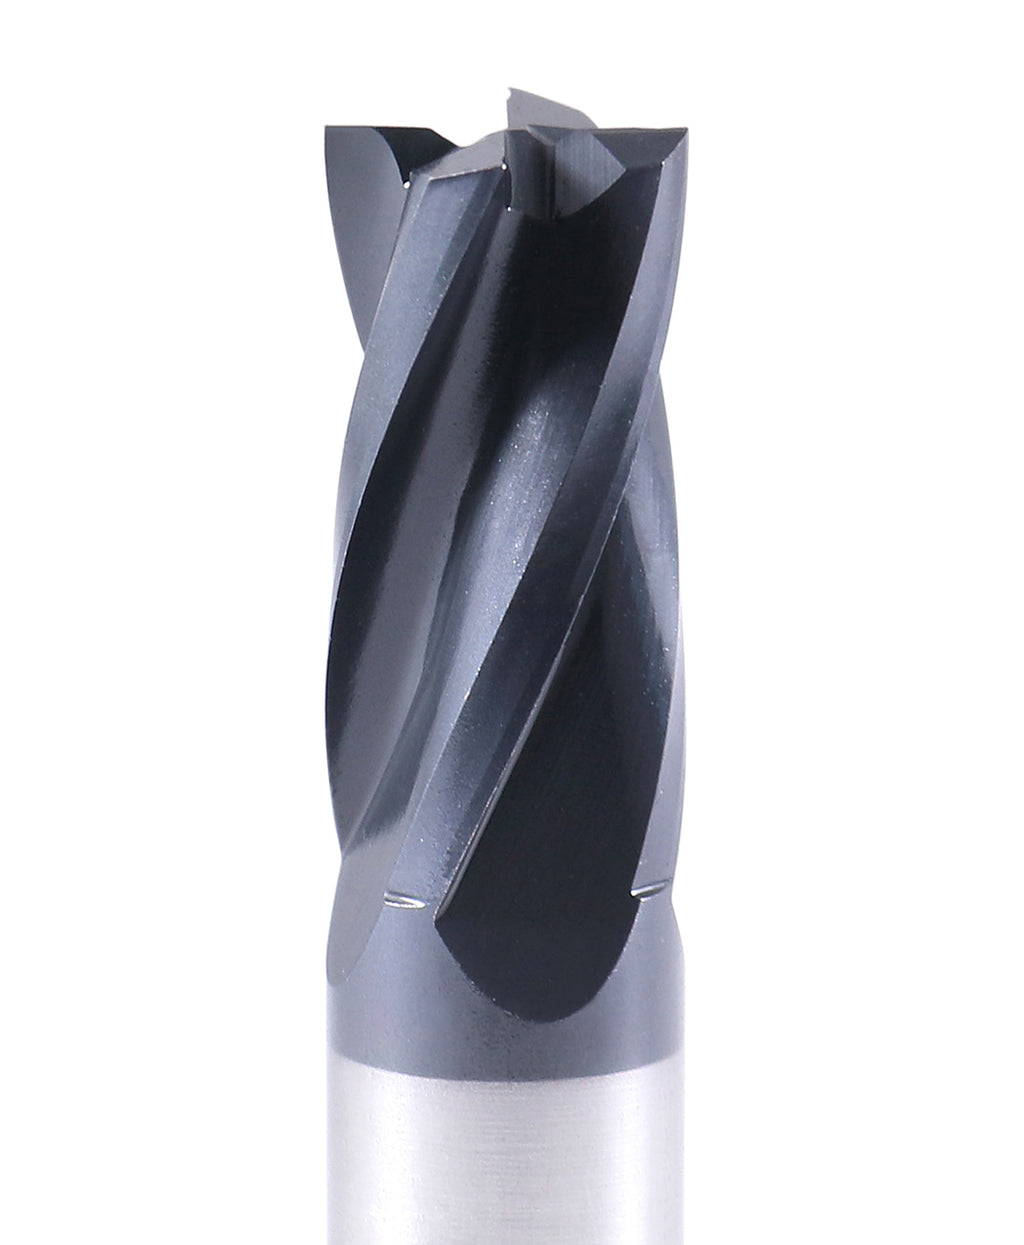
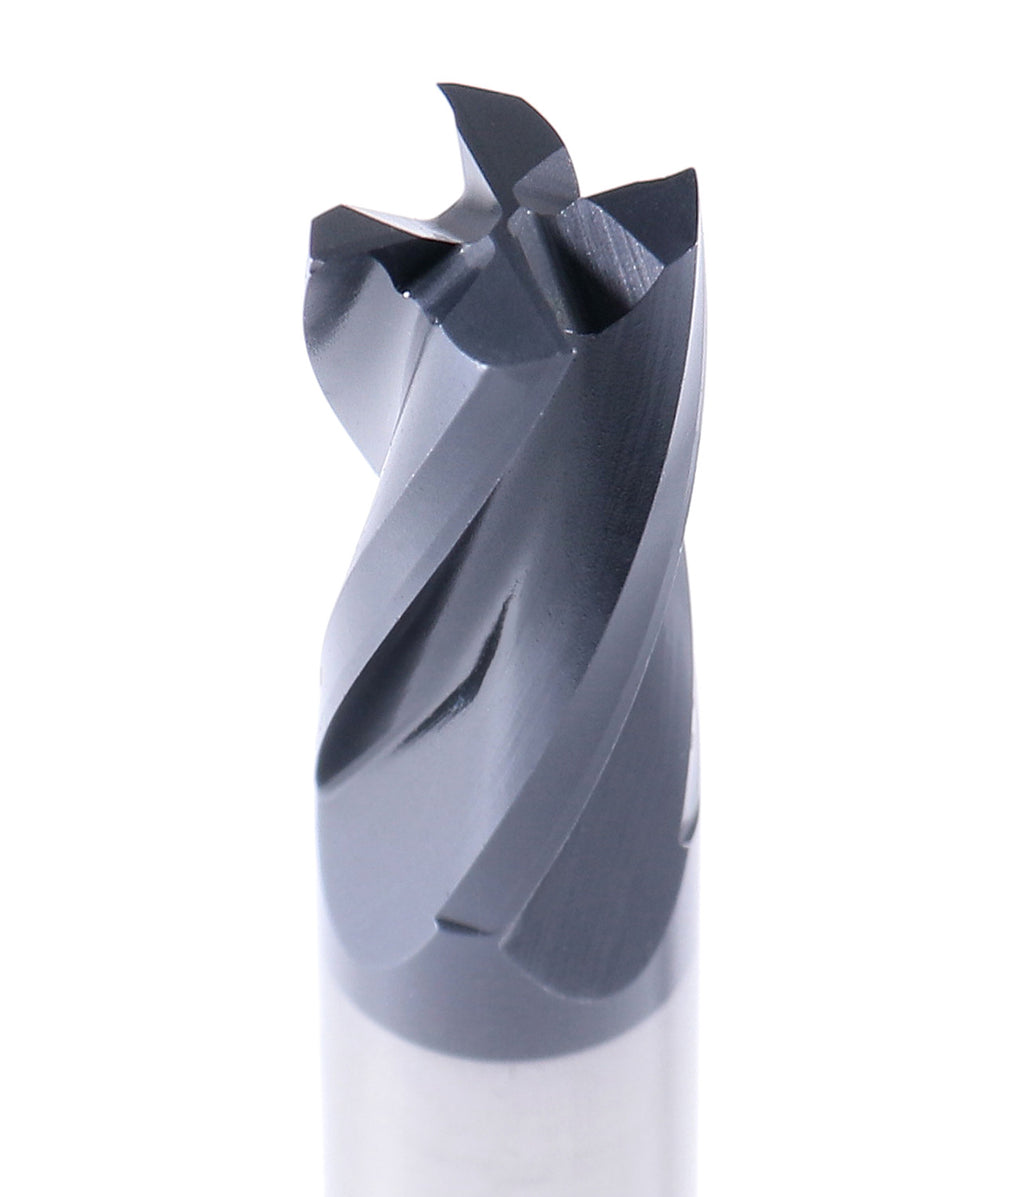
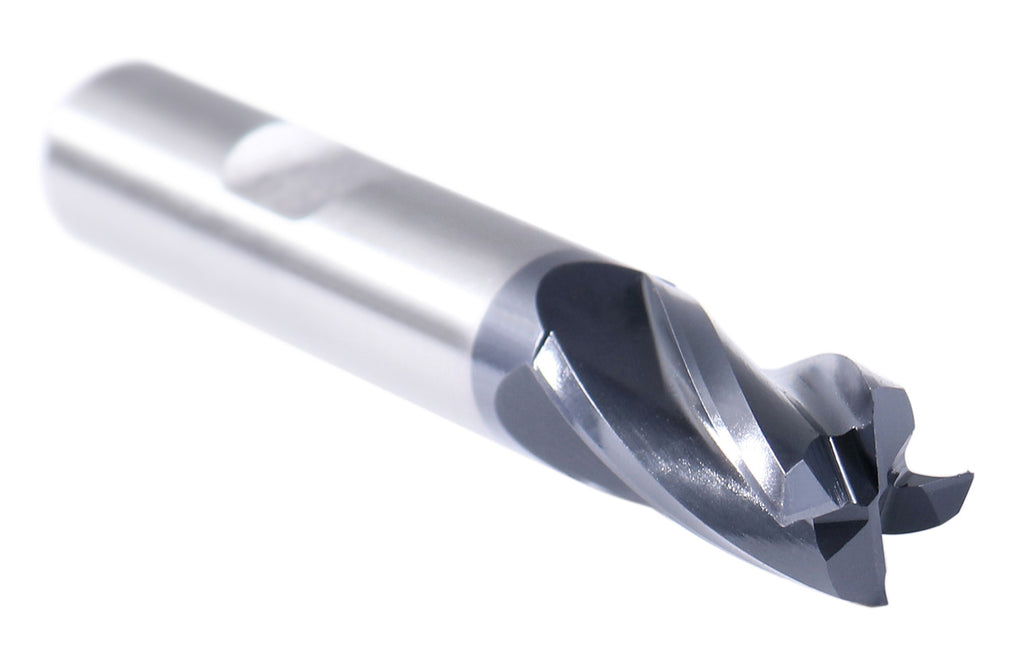
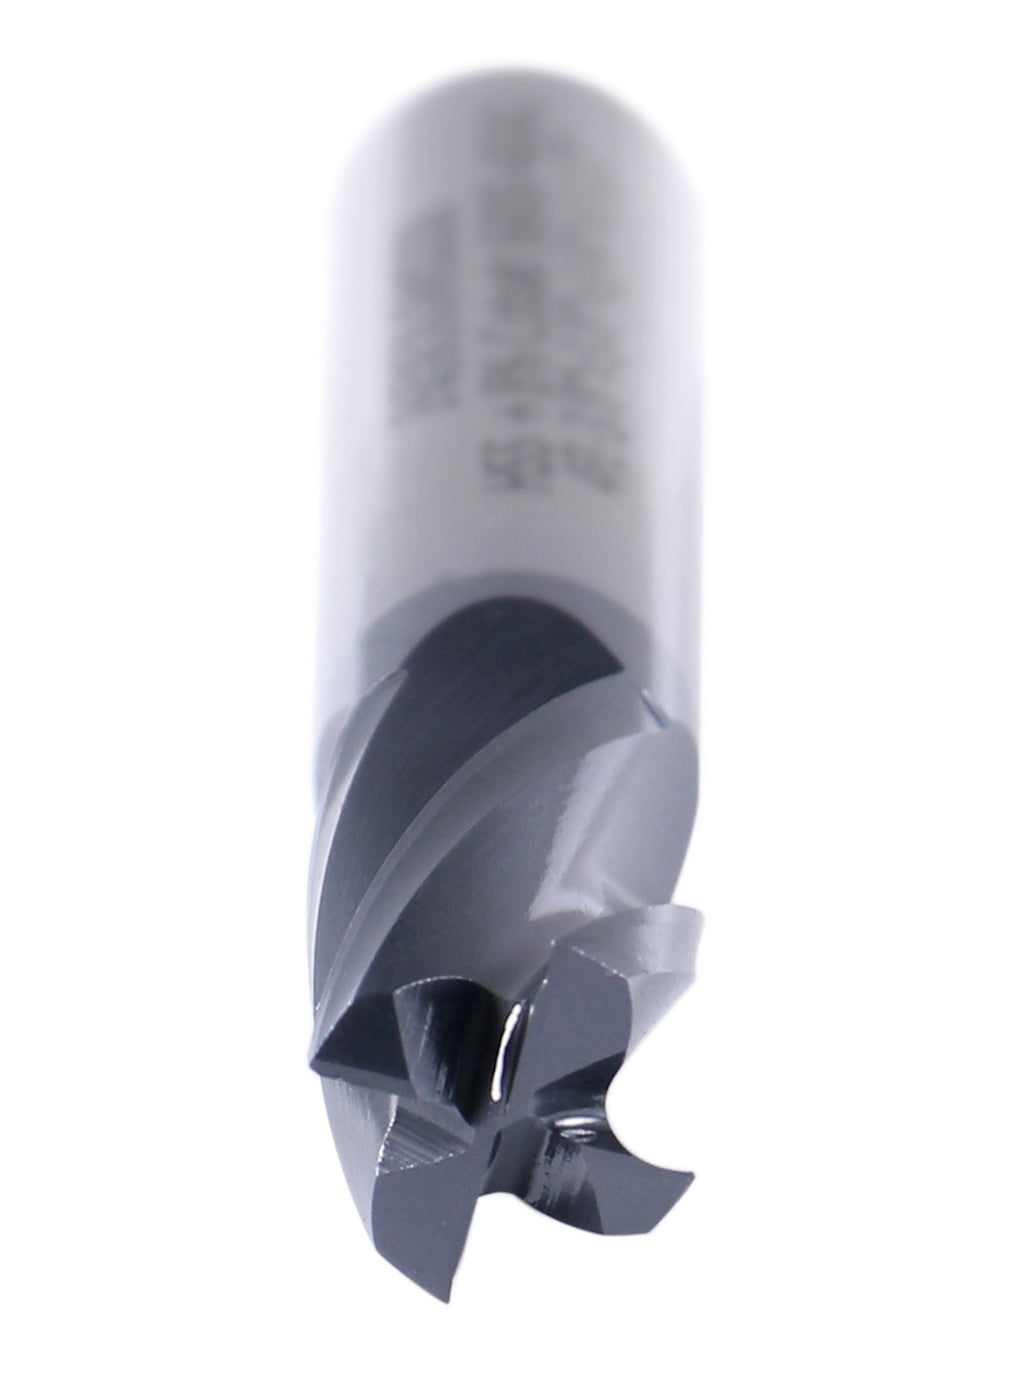
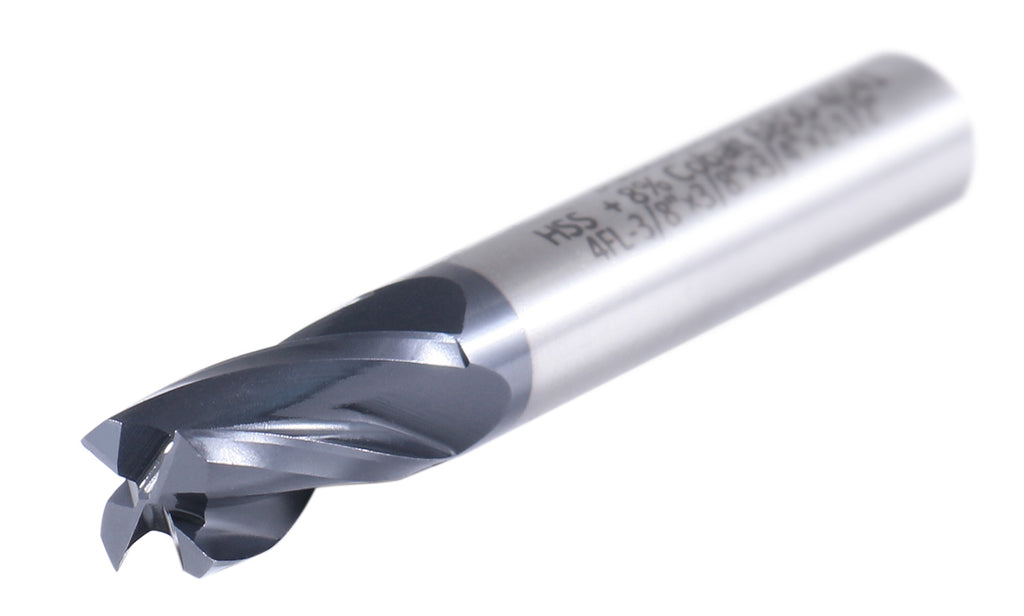
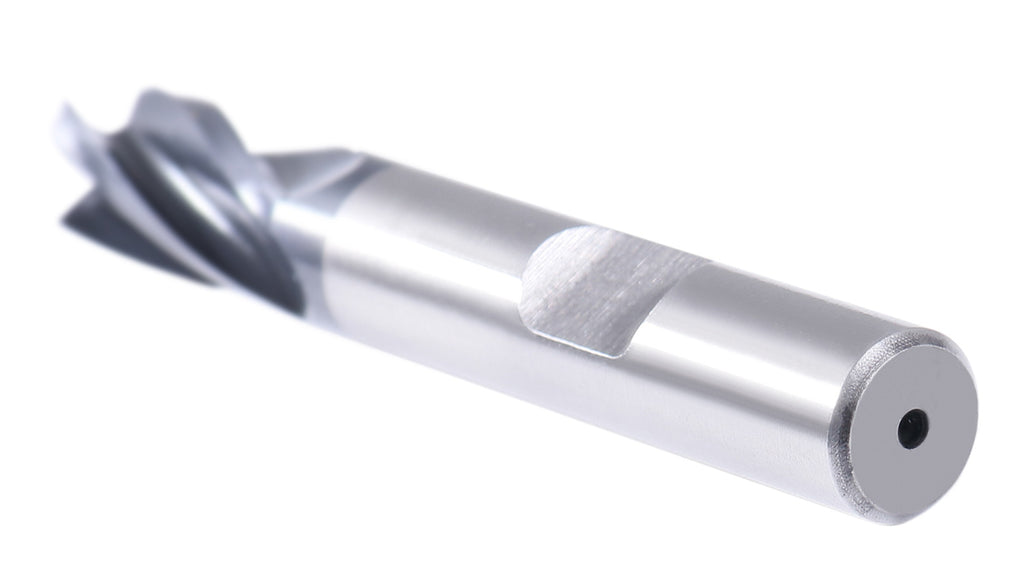
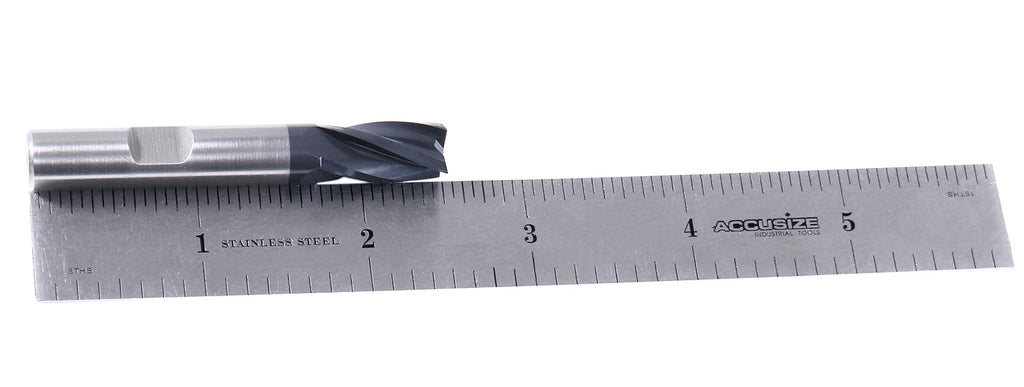
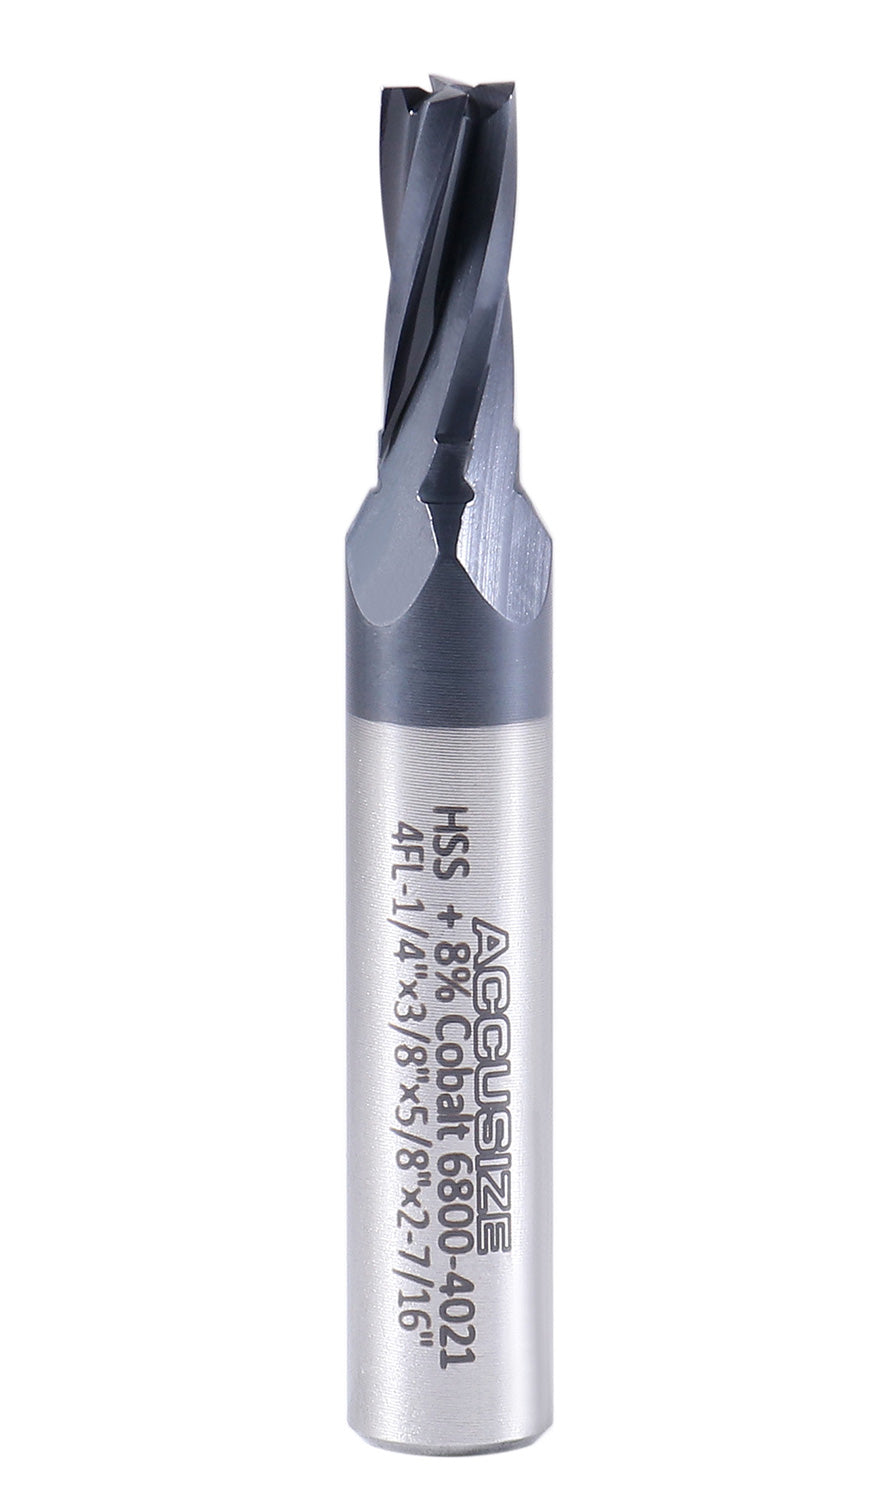
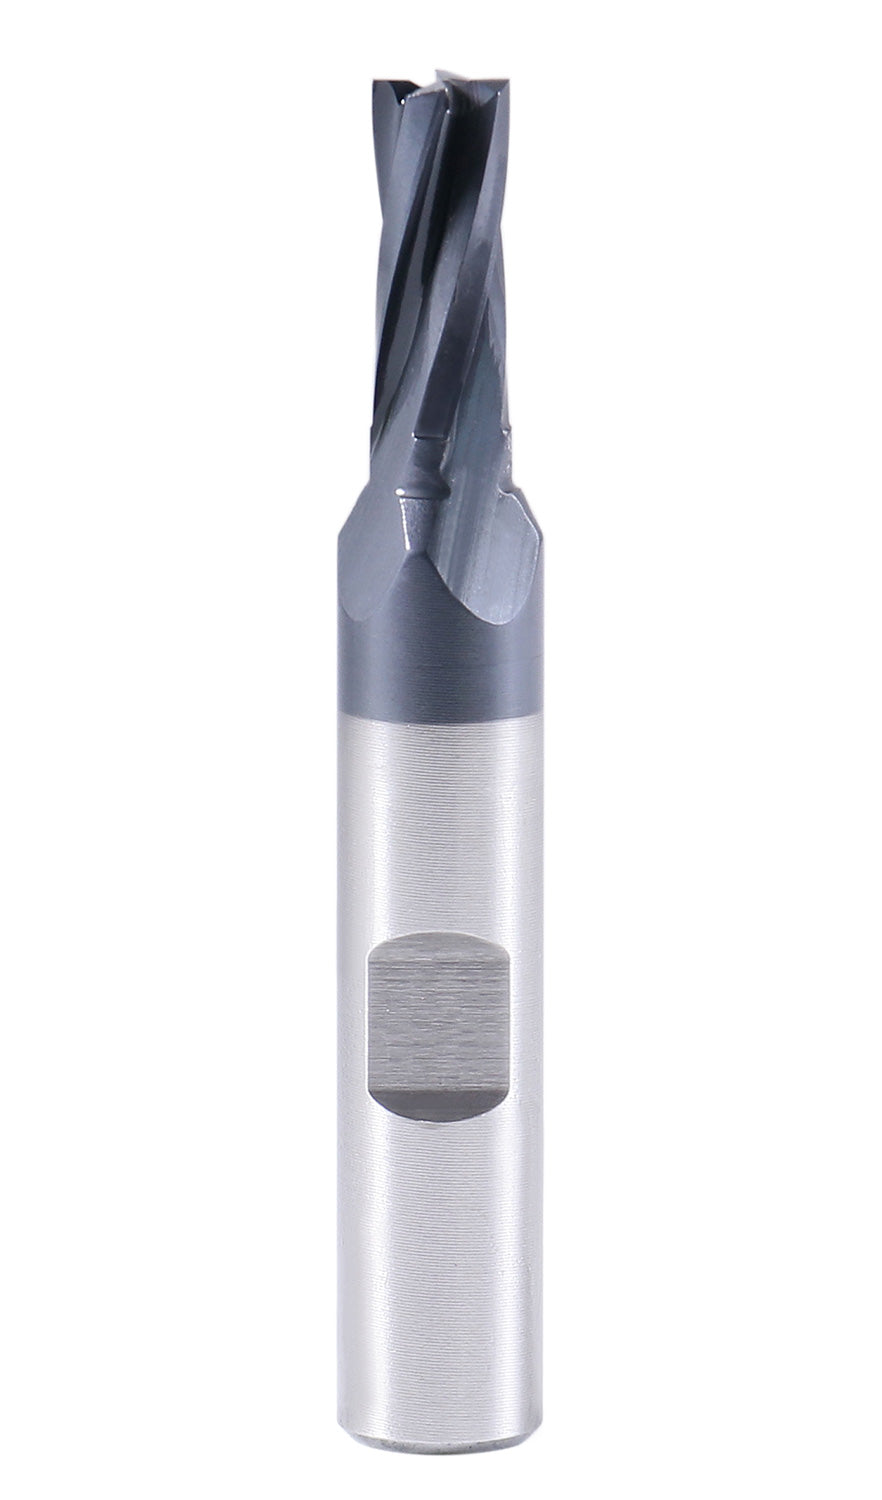
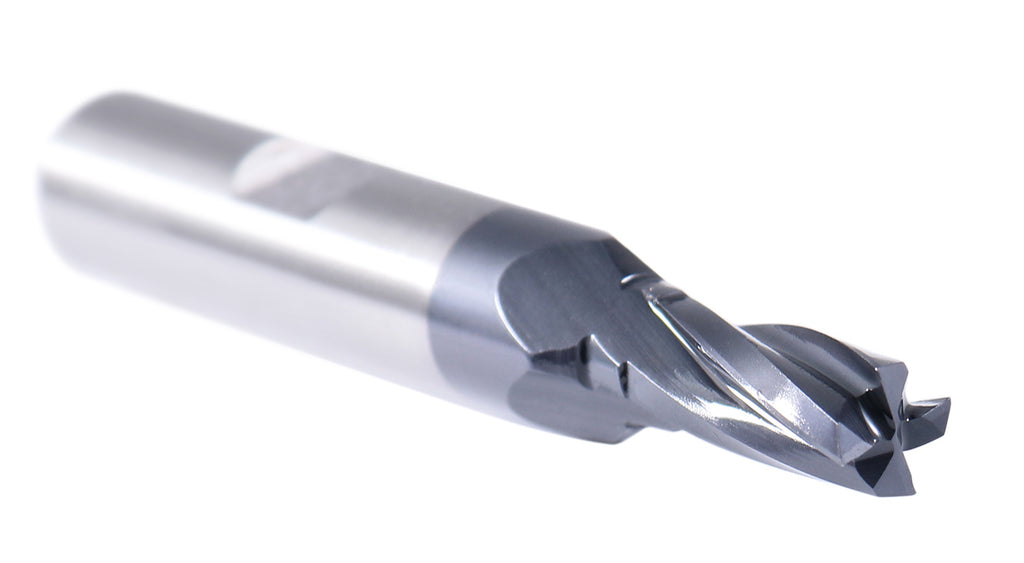
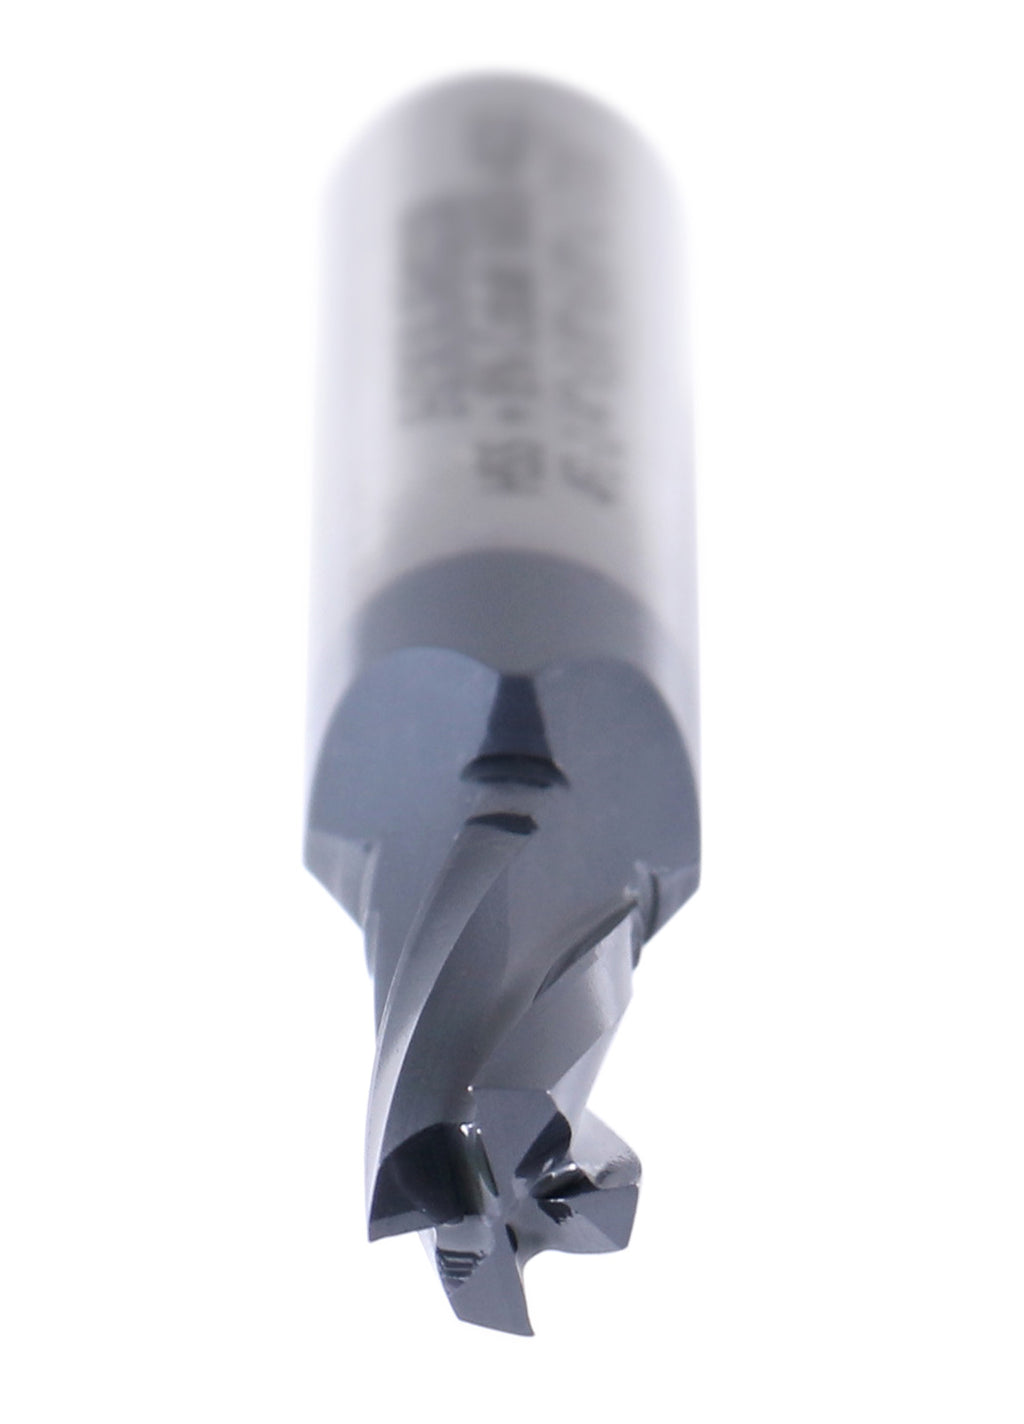
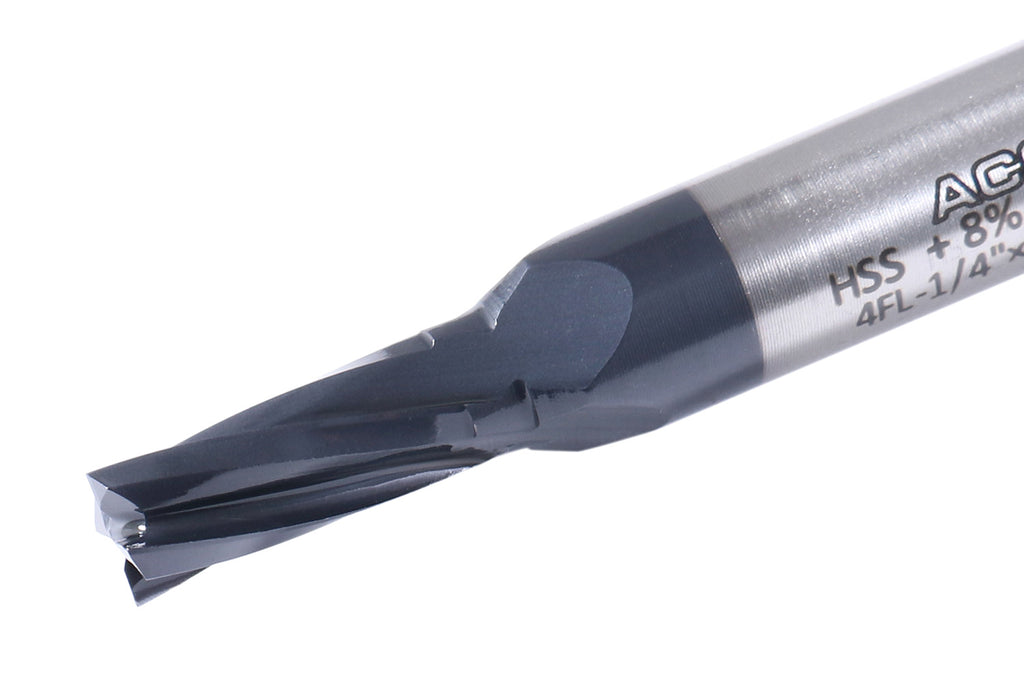
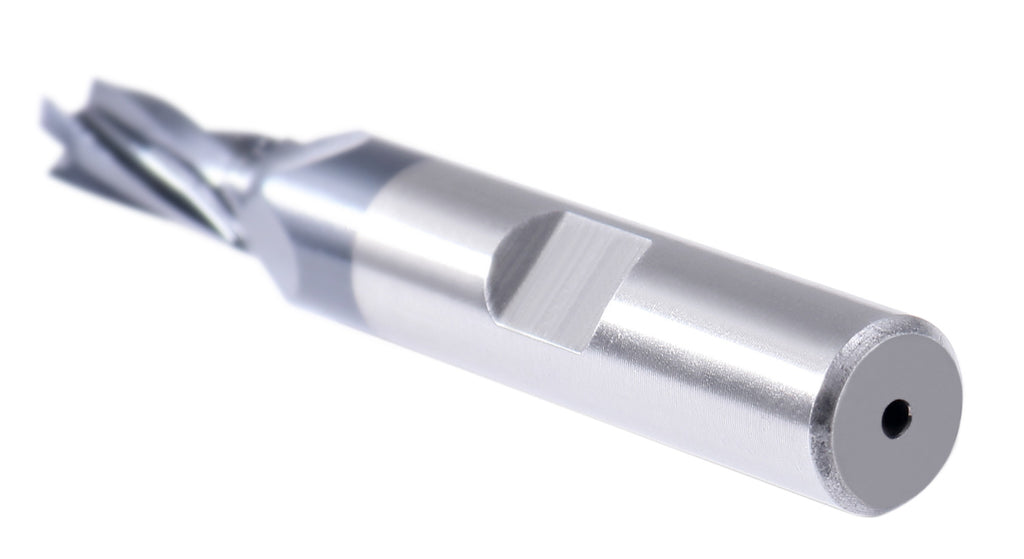
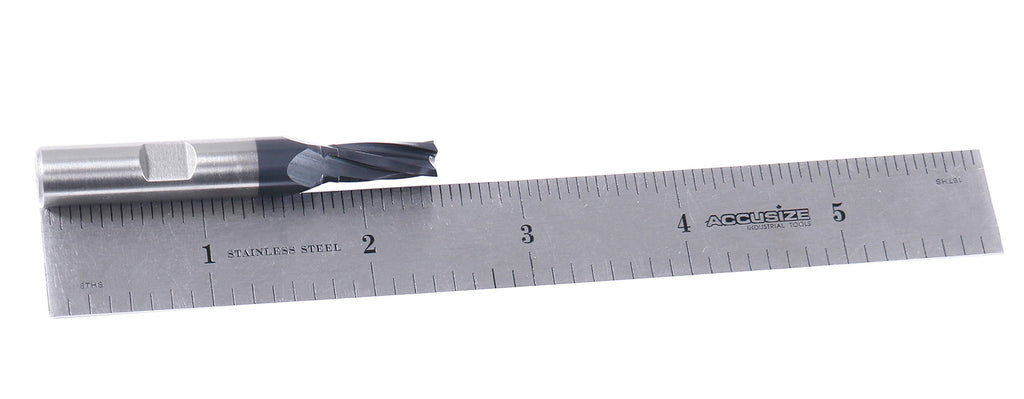
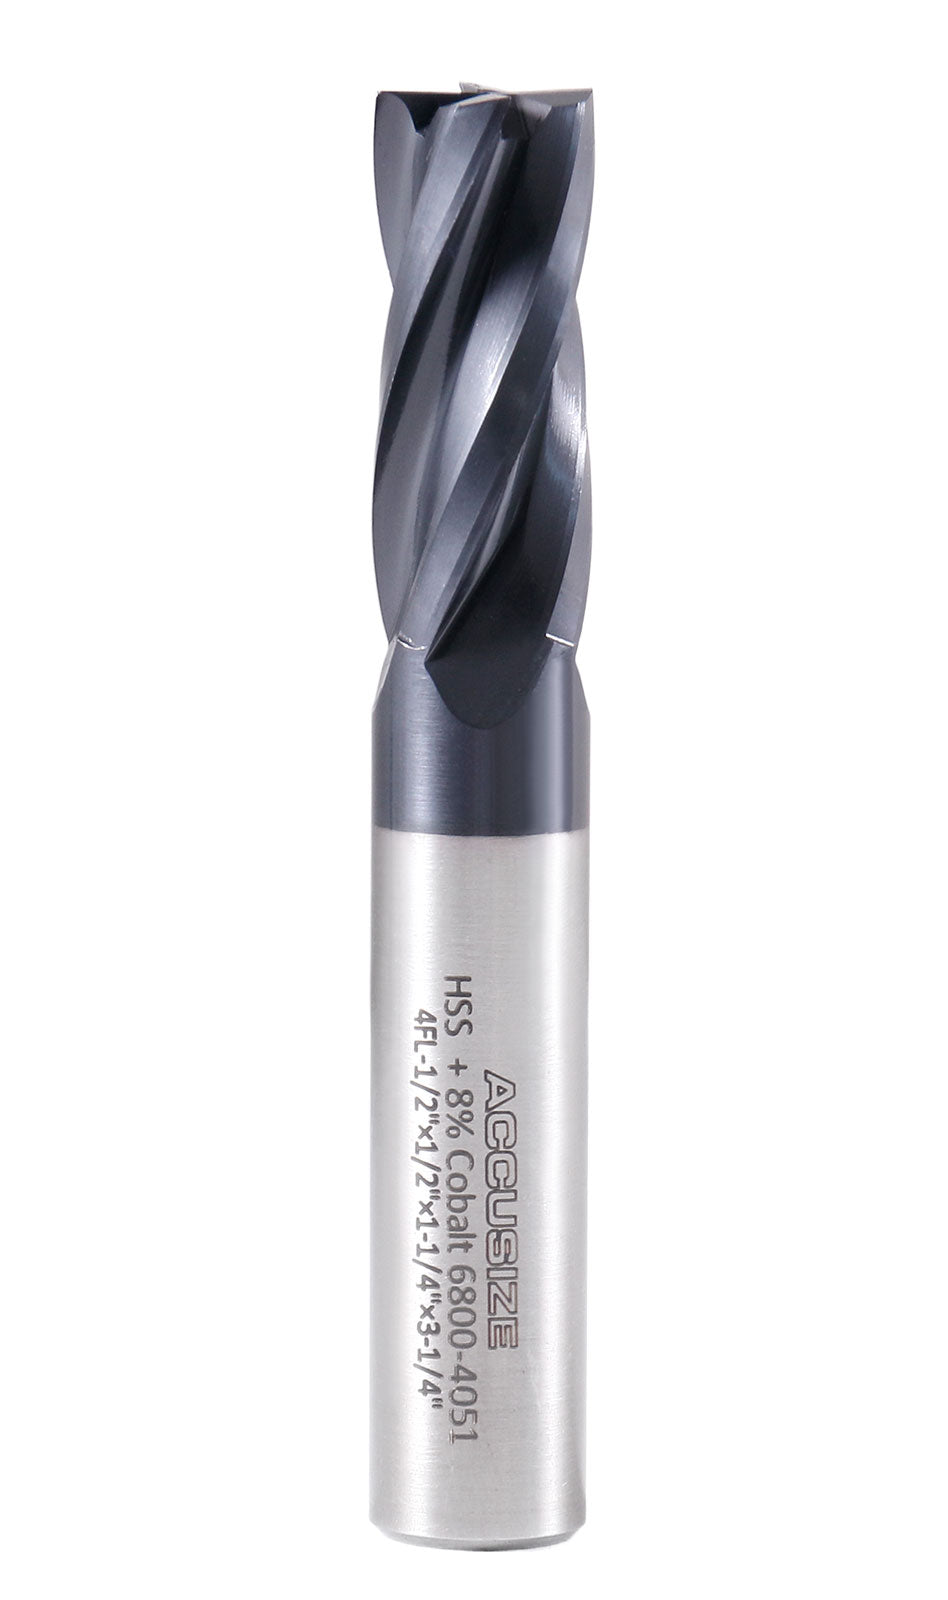
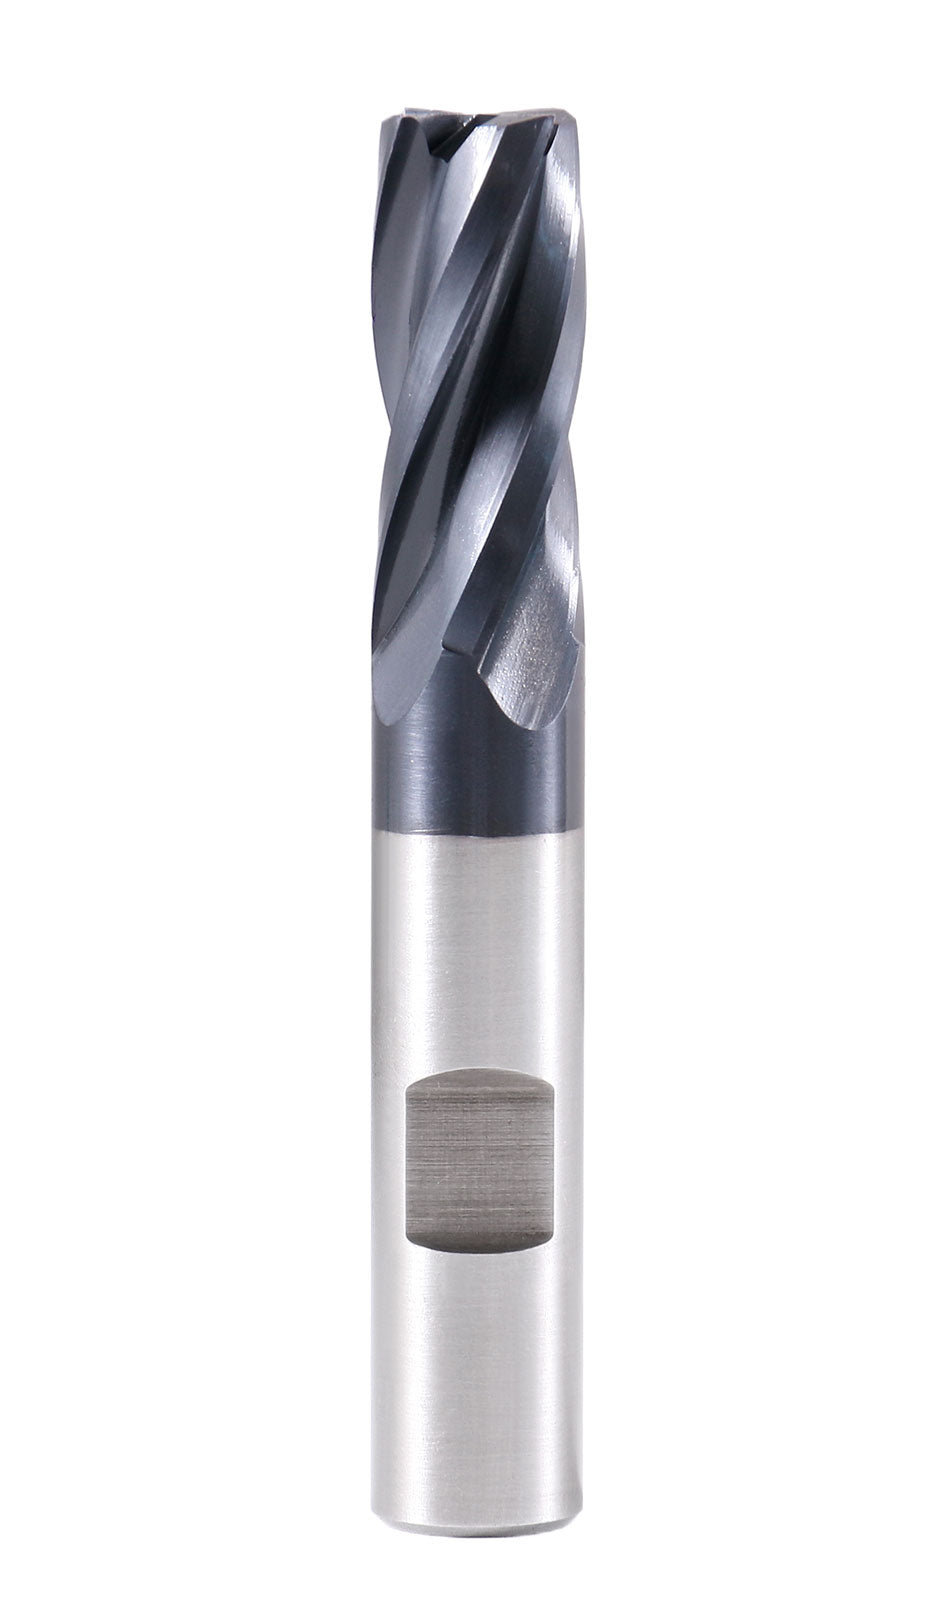
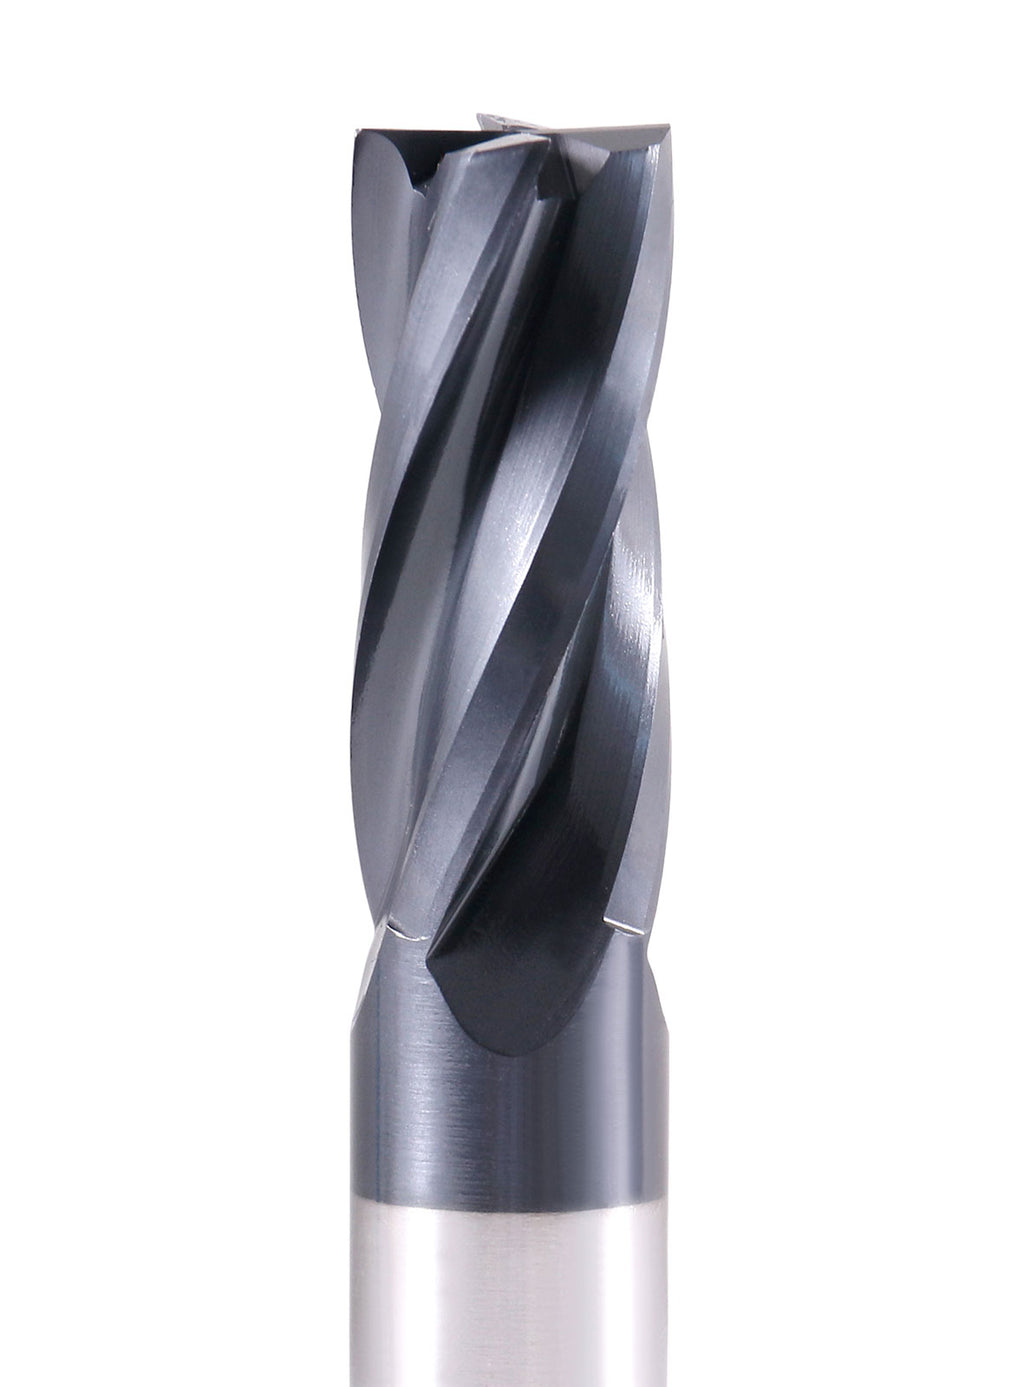
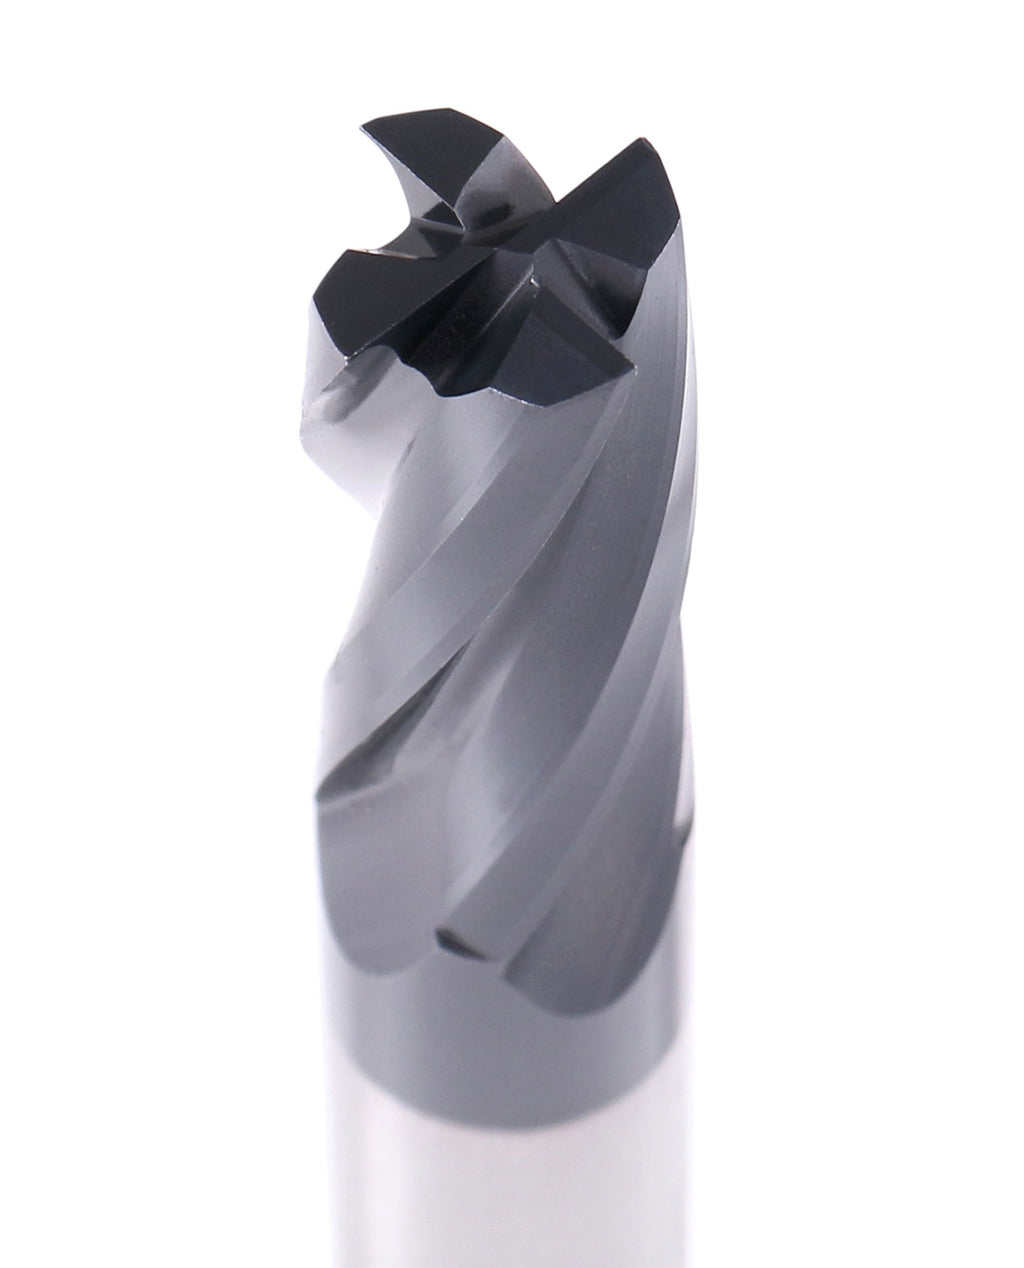
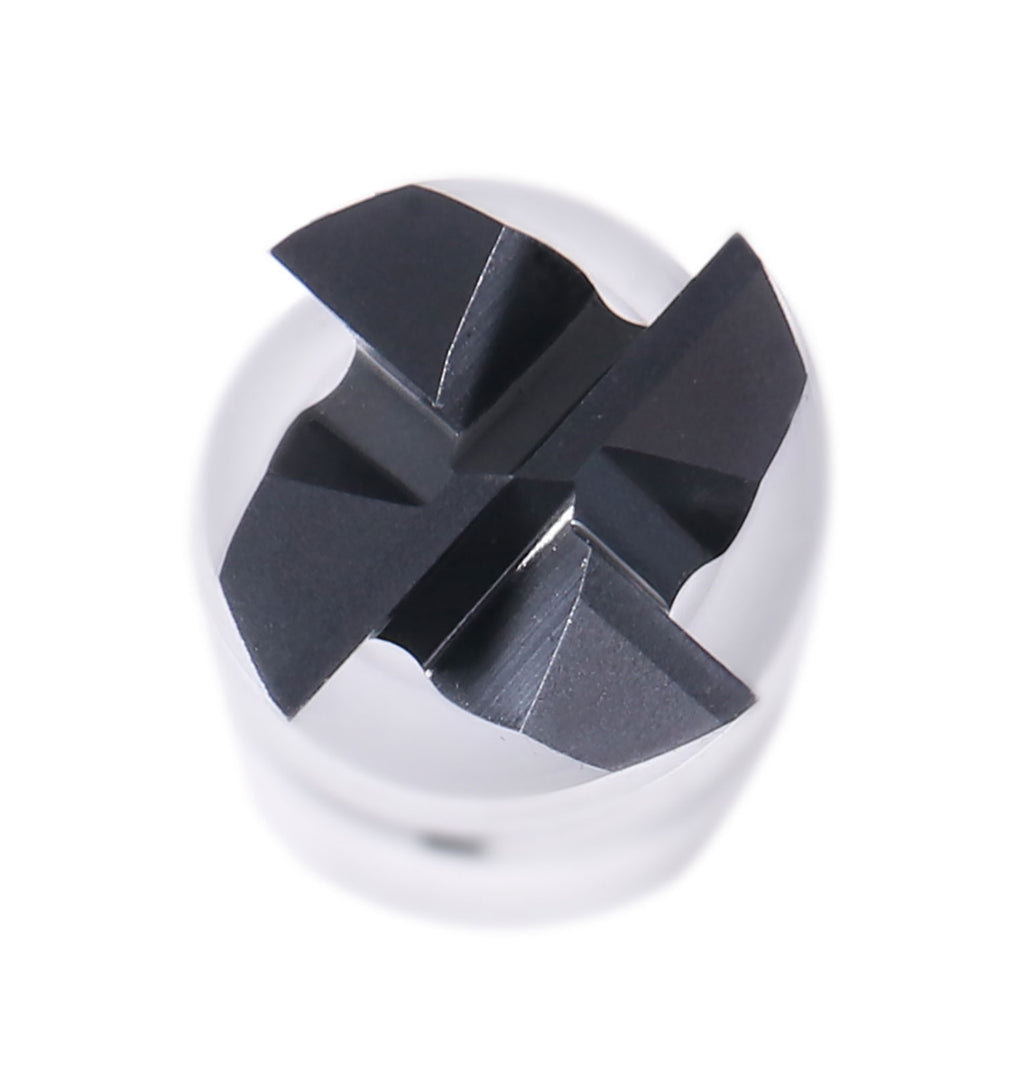
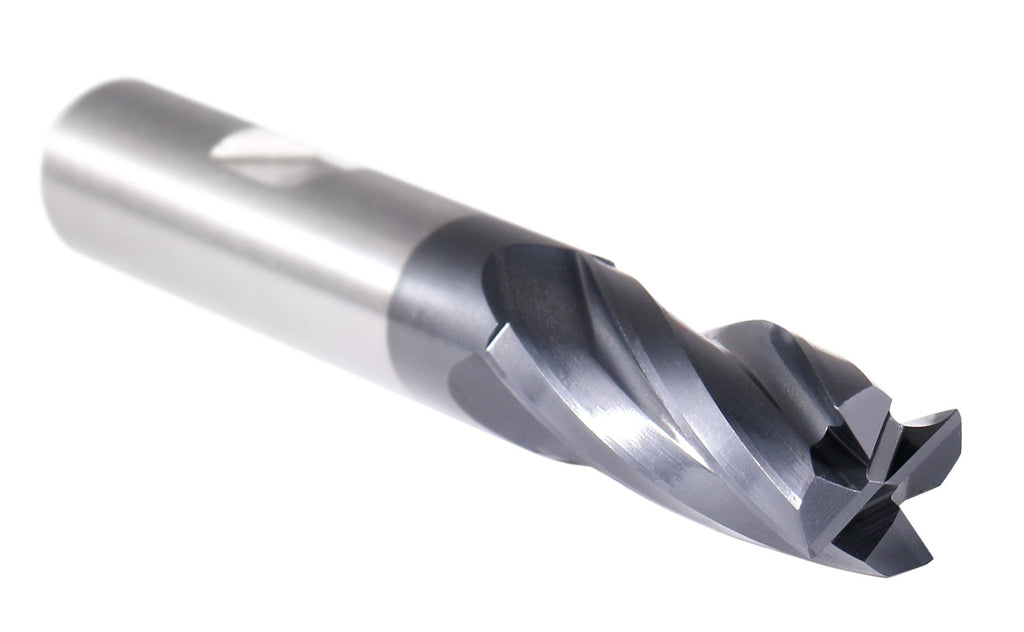
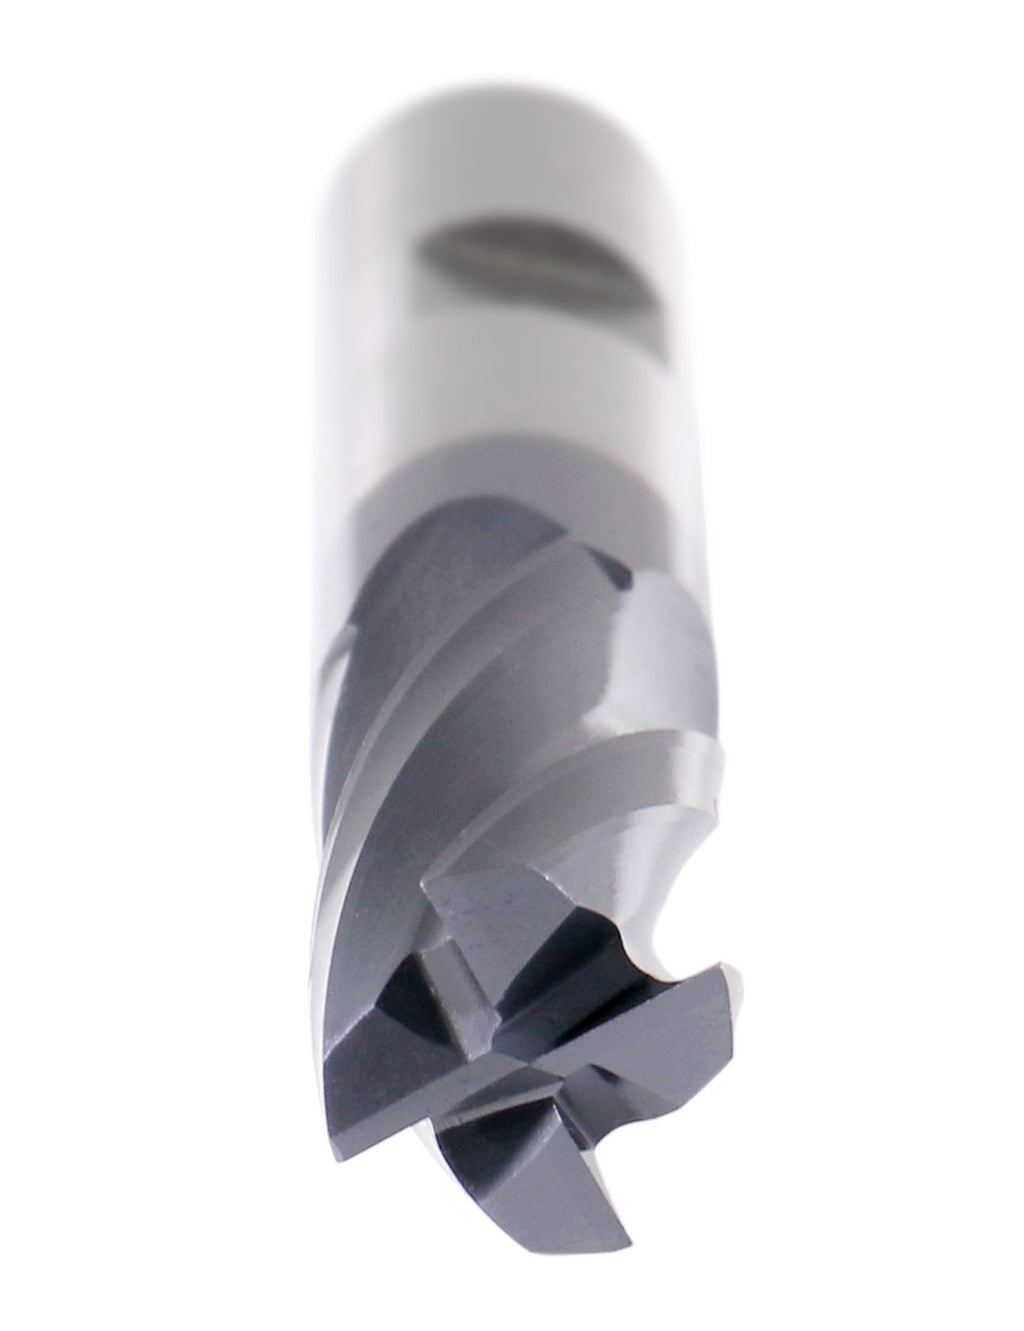
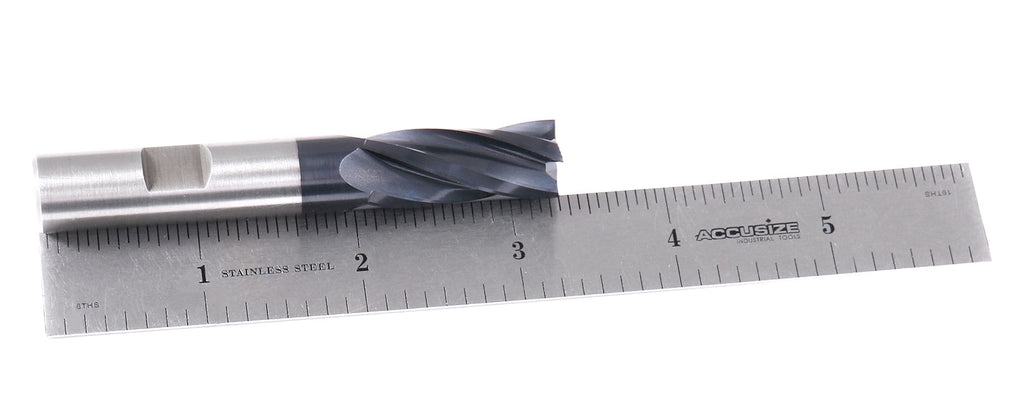
M42 (HSS+8% Cobalt) Finishing CNC End Mill, 4 Flute, TiAlN Coating
- TiAlN Coated
- Single end
- Center cutting
- M42-8% Premium cobalt
- Flutes ground by a world-class IS-9002 Factory, CNC Qualified
| Item # | Dia. | Shk. Dia. | Flt. Length | Oal. |
|---|---|---|---|---|
| 6800-4001 | 1/8" | 3/8" | 3/8" | 2-5/16" |
| 6800-4021 | 1/4" | 3/8" | 5/8" | 2-7/16" |
| 6800-4041 | 3/8" | 3/8" | 3/4" | 2-1/2" |
| 6800-4051 | 1/2" | 1/2" | 1-1/4" | 3-1/4" |
| 6800-4061 | 5/8" | 5/8" | 1-5/8" | 3-3/4" |
| 6800-4081 | 3/4" | 3/4" | 1-5/8" | 3-7/8" |
| 6800-4101 | 7/8" | 7/8" | 1-7/8" | 4-1/8" |
| 6800-4121 | 1" | 1" | 2" | 4-1/2" |

| Recommended Cutting Conditions for Roughing End Mills [Side Milling] | ||||||||||||
| Work Material |
Low Carbon Steels (Tensile Strength: ≤180N/mm2) Copper Alloys, Cast Iron(Soft) |
Medium Carbon Steels (Tensile Strength: 480-720N/mm2) Copper Alloys, Cast Iron(Hard) |
High Carbon Steels (Tensile Strength: 720-950N/mm2) Alloys Steel, Stainless Steels |
Special Alloy Steels Untree-cutting Steels (30-40HRC) |
Aluminum, Aluminum Alloys & Plastic |
|||||||
| Mill Dia | Ae | Ad | Speed | Feed | Speed | Feed | Speed | Feed | Speed | Feed | Speed | Feed |
| (inch) | (inch) | (inch) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) |
| 1/8" | 0.0125" | 3/16" | 5035 | 0.347 | 3800 | 0.265 | 2518 | 0.134 | 1520 | 0.065 | 17100 | 1.115 |
| 1/4" | 0.0250" | 3/8" | 2518 | 0.495 | 1900 | 0.370 | 1254 | 0.177 | 760 | 0.088 | 8500 | 1.394 |
| 3/8" | 0.0375" | 9/16" | 1425 | 0.662 | 1064 | 0.495 | 713 | 0.236 | 428 | 0.121 | 4750 | 1.742 |
| 1/2" | 0.0500" | 3/4" | 1121 | 0.626 | 855 | 0.469 | 570 | 0.223 | 337 | 0.121 | 3800 | 1.646 |
| 5/8" | 1/16" | 15/16" | 903 | 0.557 | 675 | 0.419 | 451 | 0.223 | 266 | 0.124 | 2992 | 1.479 |
| 3/4" | 0.0750" | 1-1/8" | 713 | 0.524 | 532 | 0.347 | 356 | 0.209 | 190 | 0.111 | 2375 | 1.394 |
| 7/8" | 0.0875" | 1-5/16" | 637 | 0.495 | 475 | 0.311 | 318 | 0.183 | 171 | 0.101 | 1900 | 1.184 |
| 1" | 0.1000" | 1-1/2" | 570 | 0.469 | 428 | 0.278 | 285 | 0.164 | 152 | 0.088 | 1710 | 1.115 |

- The Indicated speeds and feeds are
- For side milling with 2‐fluted end mill to a depth=0.1xD and a width of cut=1.5xD
- For milling with 4‐fluted, the feed should be twice that listed above.
- For finishing operations, the feed should be increased by 30�0%. 3.Use a rigid and precise machine and holder.
- Use suitable cutting fluids
| Recommended Cutting Conditions for Roughing End Mills [Side Milling] | ||||||||||||
| Work Material |
Low Carbon Steels (Tensile Strength: ≤180N/mm2) Copper Alloys, Cast Iron(Soft) |
Medium Carbon Steels (Tensile Strength: 480-720N/mm2) Copper Alloys, Cast Iron(Hard) |
High Carbon Steels (Tensile Strength: 720-950N/mm2) Alloys Steel, Stainless Steels |
Special Alloy Steels Untree-cutting Steels (30-40HRC) |
Aluminium, Aluminium Alloys & Plastic |
|||||||
| Mill Dia | Ad | Speed | Feed | Speed | Feed | Speed | Feed | Speed | Feed | Speed | Feed | |
| (inch) | (inch) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | (rpm) | ( ft /min) | |
| 1/8" | 1/32" | 4275 | 0.590 | 3192 | 0.419 | 1900 | 0.203 | 1330 | 0.111 | 10640 | 1.397 | |
| 1/4" | 1/16" | 2128 | 0.839 | 1615 | 0.557 | 950 | 0.369 | 675 | 0.157 | 5320 | 1.758 | |
| 3/8" | 3/32" | 1186 | 1.115 | 903 | 0.734 | 532 | 0.354 | 380 | 0.209 | 2992 | 2.230 | |
| 1/2" | 1/8" | 950 | 1.062 | 713 | 0.656 | 428 | 0.334 | 299 | 0.209 | 2375 | 2.093 | |
| 5/8" | 5/32" | 760 | 0.951 | 570 | 0.623 | 337 | 0.334 | 238 | 0.223 | 1900 | 1.922 | |
| 3/4" | 3/16" | 599 | 0.892 | 451 | 0.531 | 266 | 0.314 | 190 | 0.223 | 1520 | 1.758 | |
| 7/8" | 7/32" | 532 | 0.839 | 404 | 0.472 | 238 | 0.282 | 171 | 0.203 | 1330 | 1.673 | |
| 1" | 1/4" | 475 | 0.780 | 356 | 0.419 | 213 | 0.249 | 152 | 0.177 | 1188 | 1.561 | |
Ad=1/4D
- The Indicated speeds and feeds are for slotting
- depth=1/4xD
- For deeper slotting , the speed should be decreased by 20-50%
- Use a rigid and precise machine and holder.
- Use suitable cutting fluids
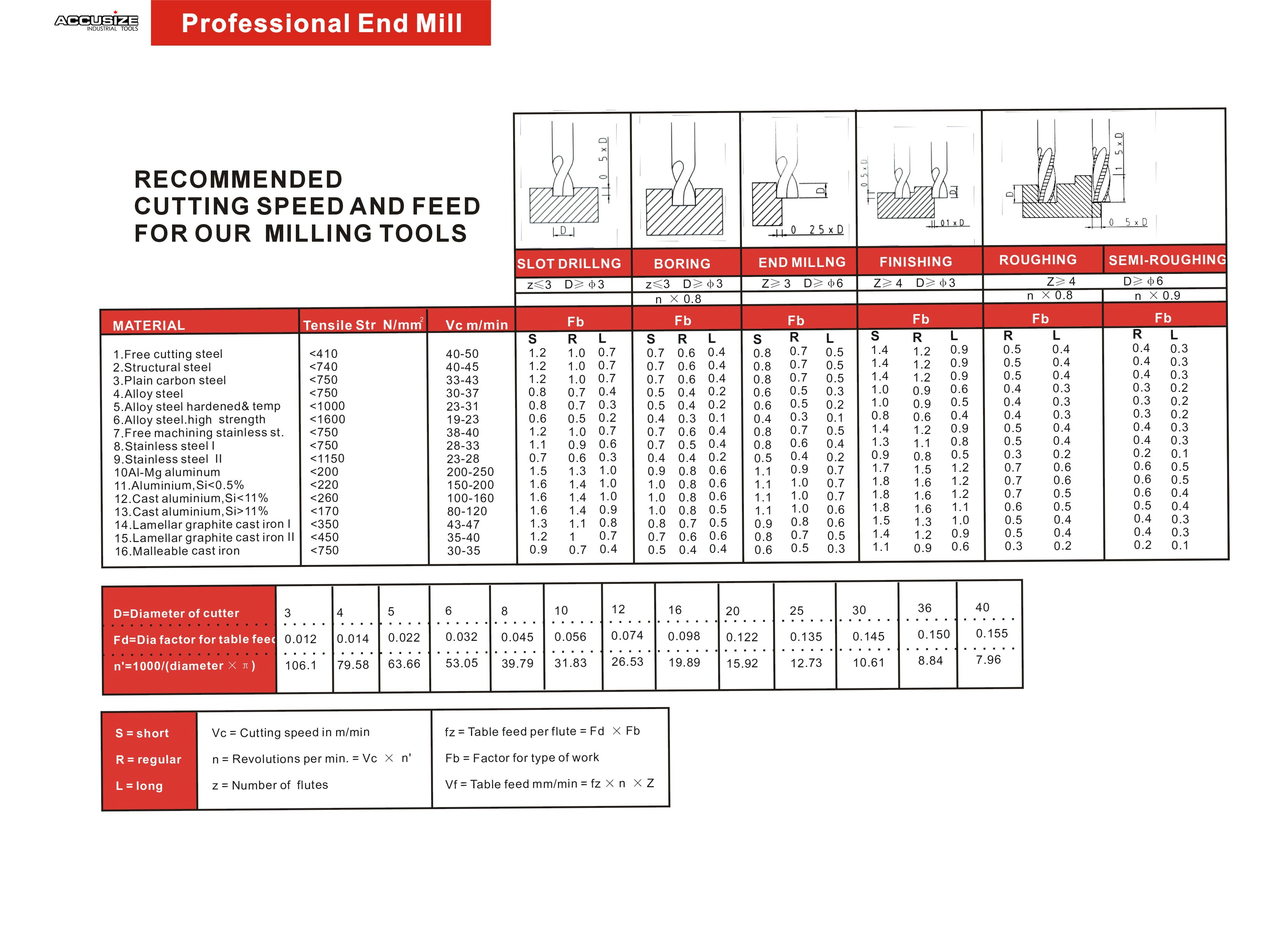
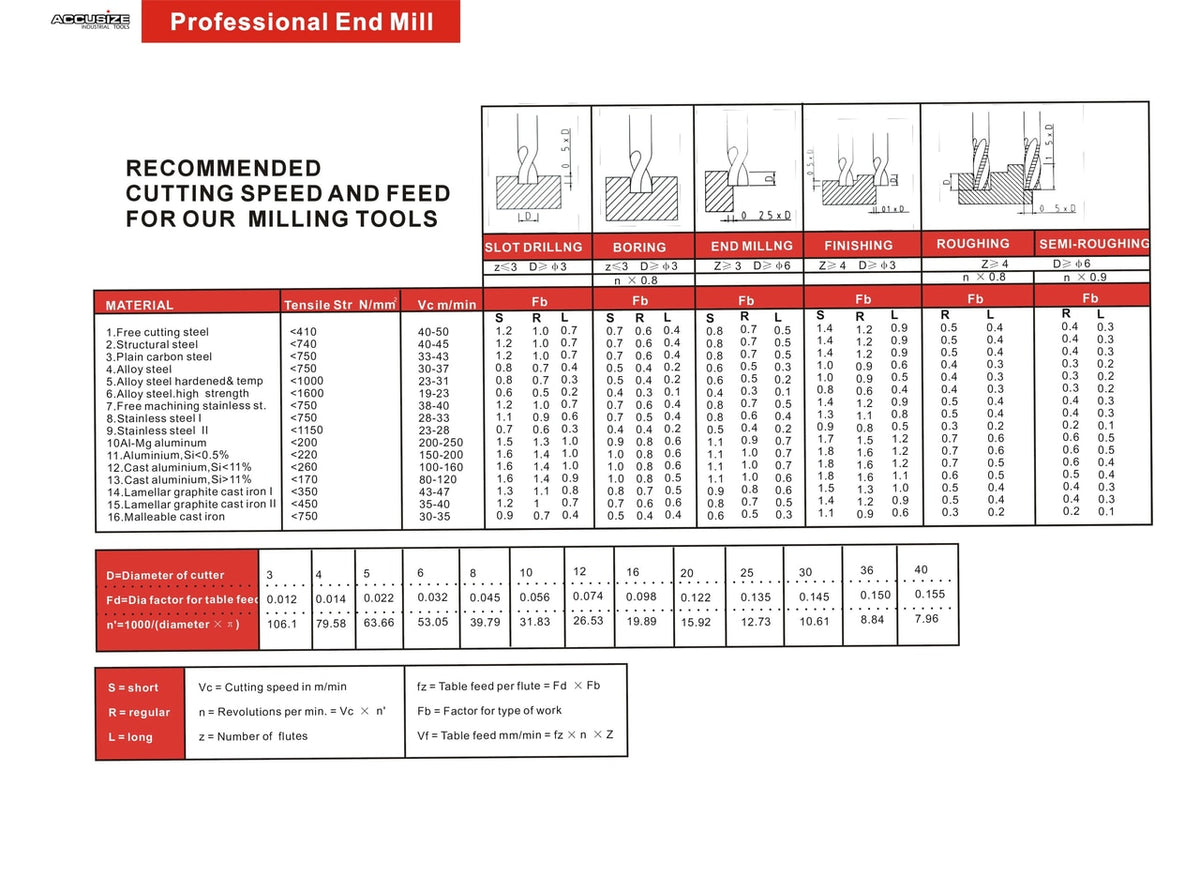
**ABOVE CUTTING PARAMETERS PROVIDED FOR REFERENCE ONLY **


Accusize Industrial Tools
ISO40 Support de fraises avec filetage 5/8"-11
Prix réduitA partir de $72.00






Accusize Industrial Tools
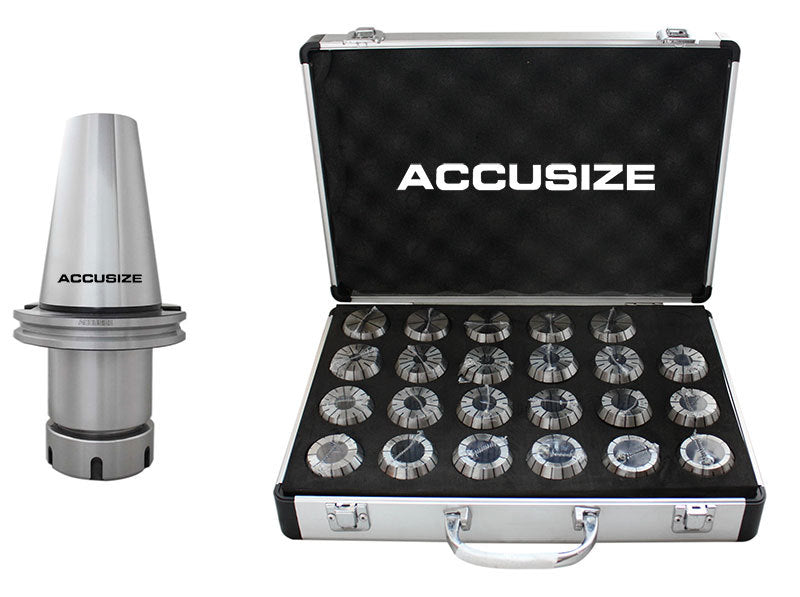
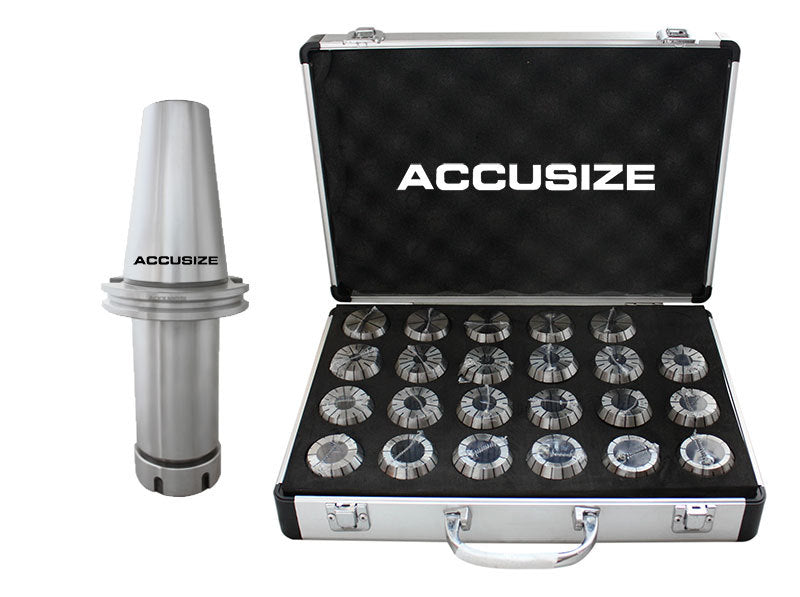
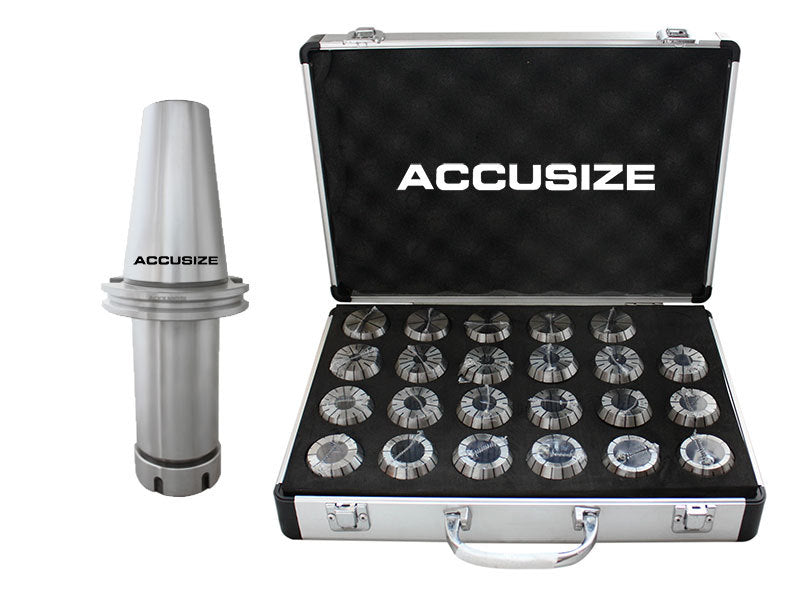
Systèmes de pince ER avec tiges CAT40 ou BT40
Prix réduitA partir de $314.00




CLEARANCE
Economisez $39.30


Accusize Industrial Tools
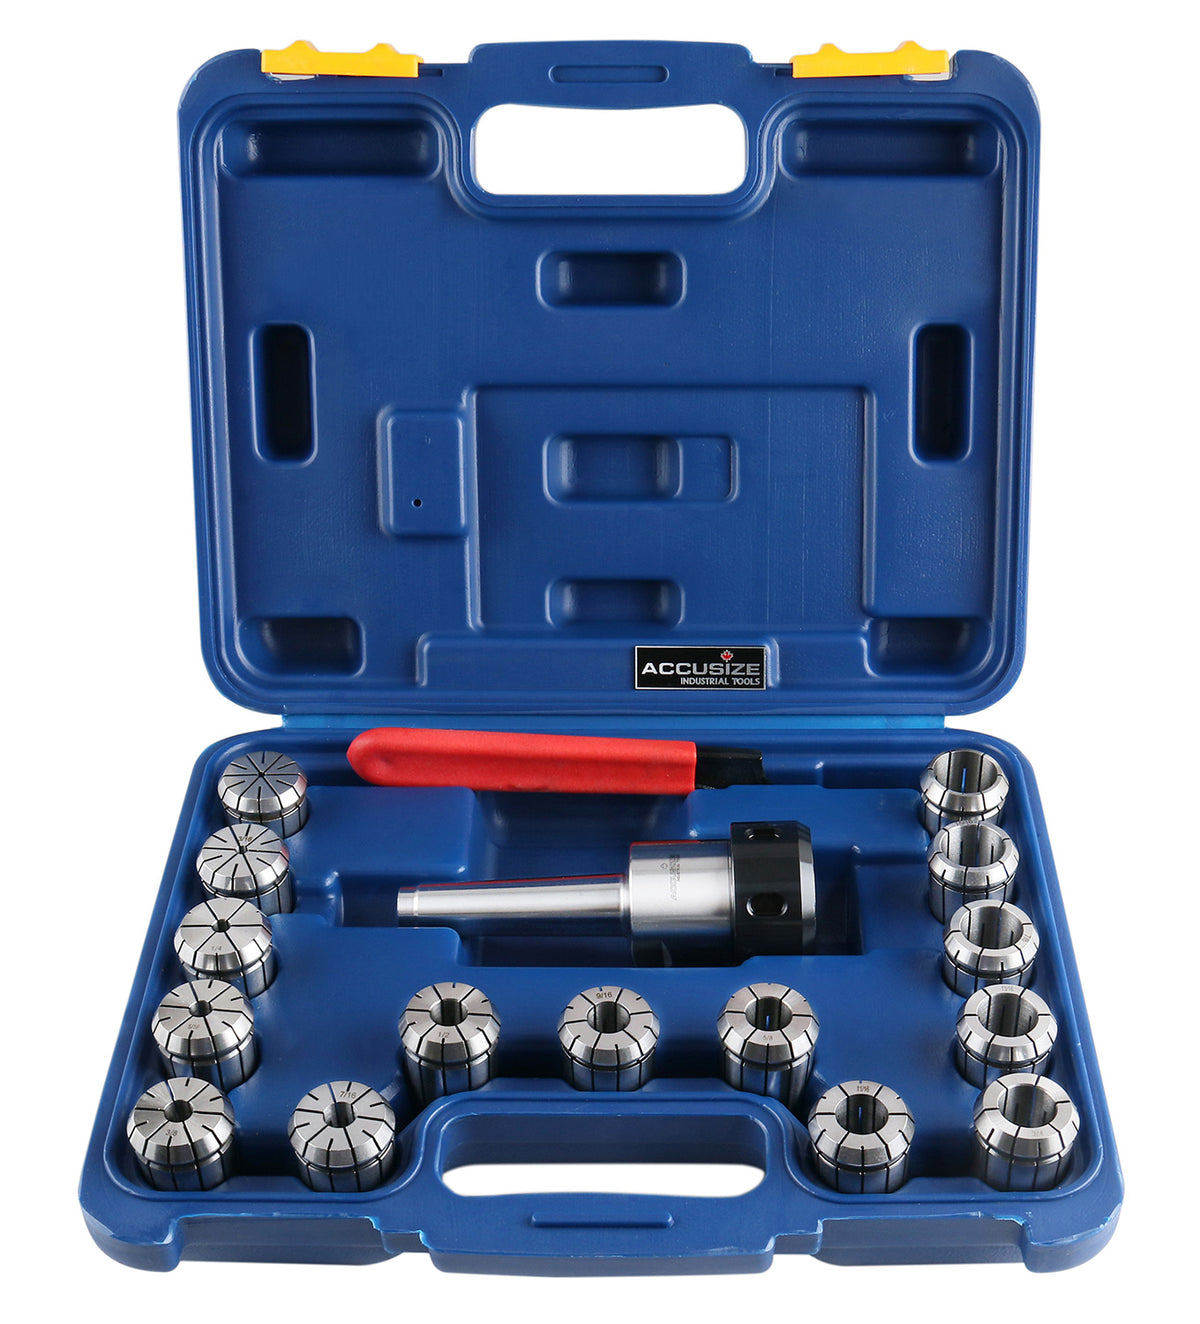
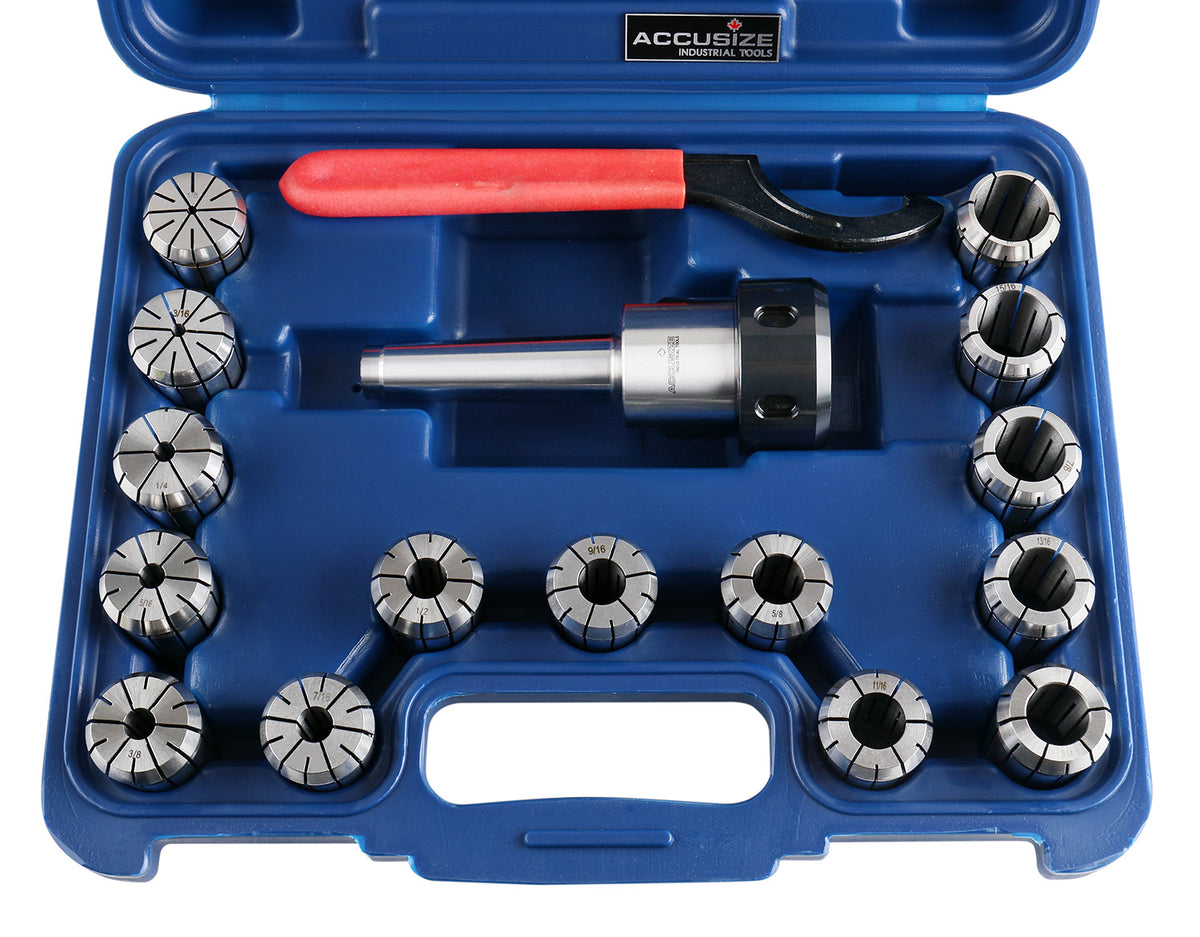
Mandrin ER32 à tige droite de 3/4'' avec kit de pinces 11pc, 1/8-3/4 par 16th, #0223 -0305
Prix réduit$222.70
Prix normal$262.00


CLEARANCE
Economisez $48.90


Accusize Industrial Tools
Mandrin ER40 à tige 5C avec jeu de 15 pinces, 1/8" - 1" par 16ème, #0223 -0302
Prix réduit$277.10
Prix normal$326.00


